EN


- Overview
- Recommended Products
RO Reverse Osmosis Systems for Food Processing Water Treatment
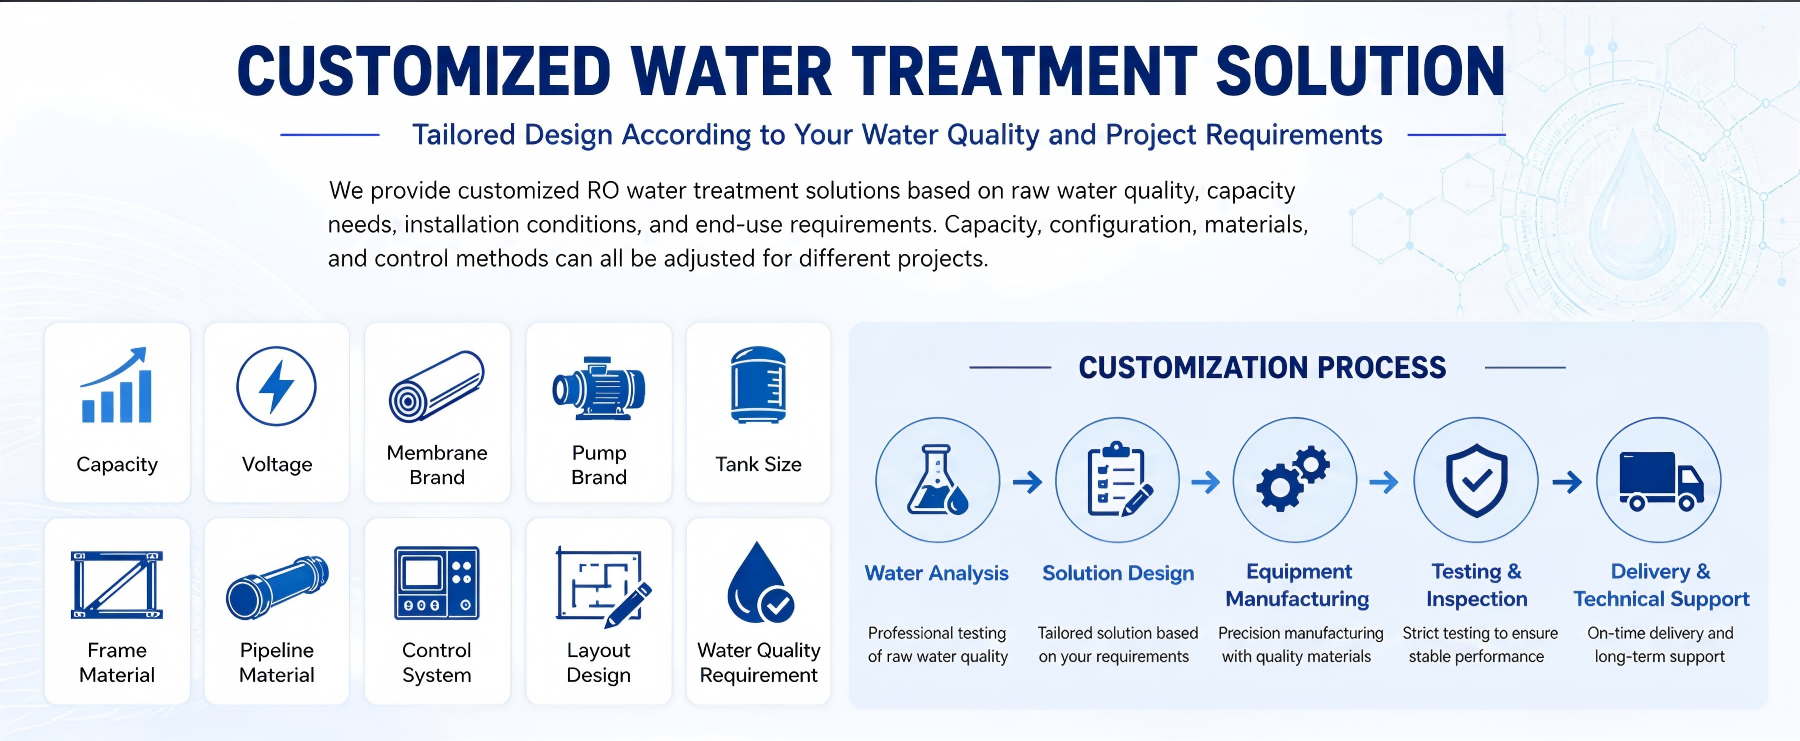
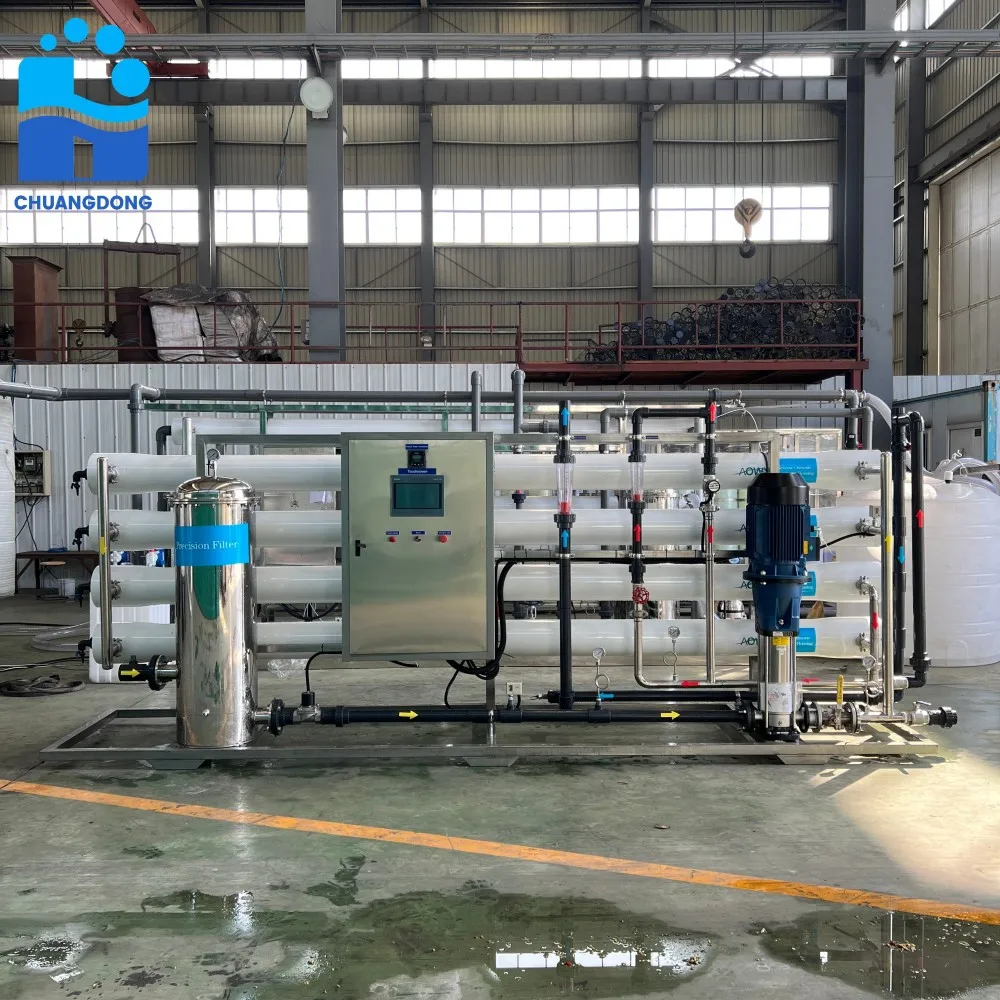
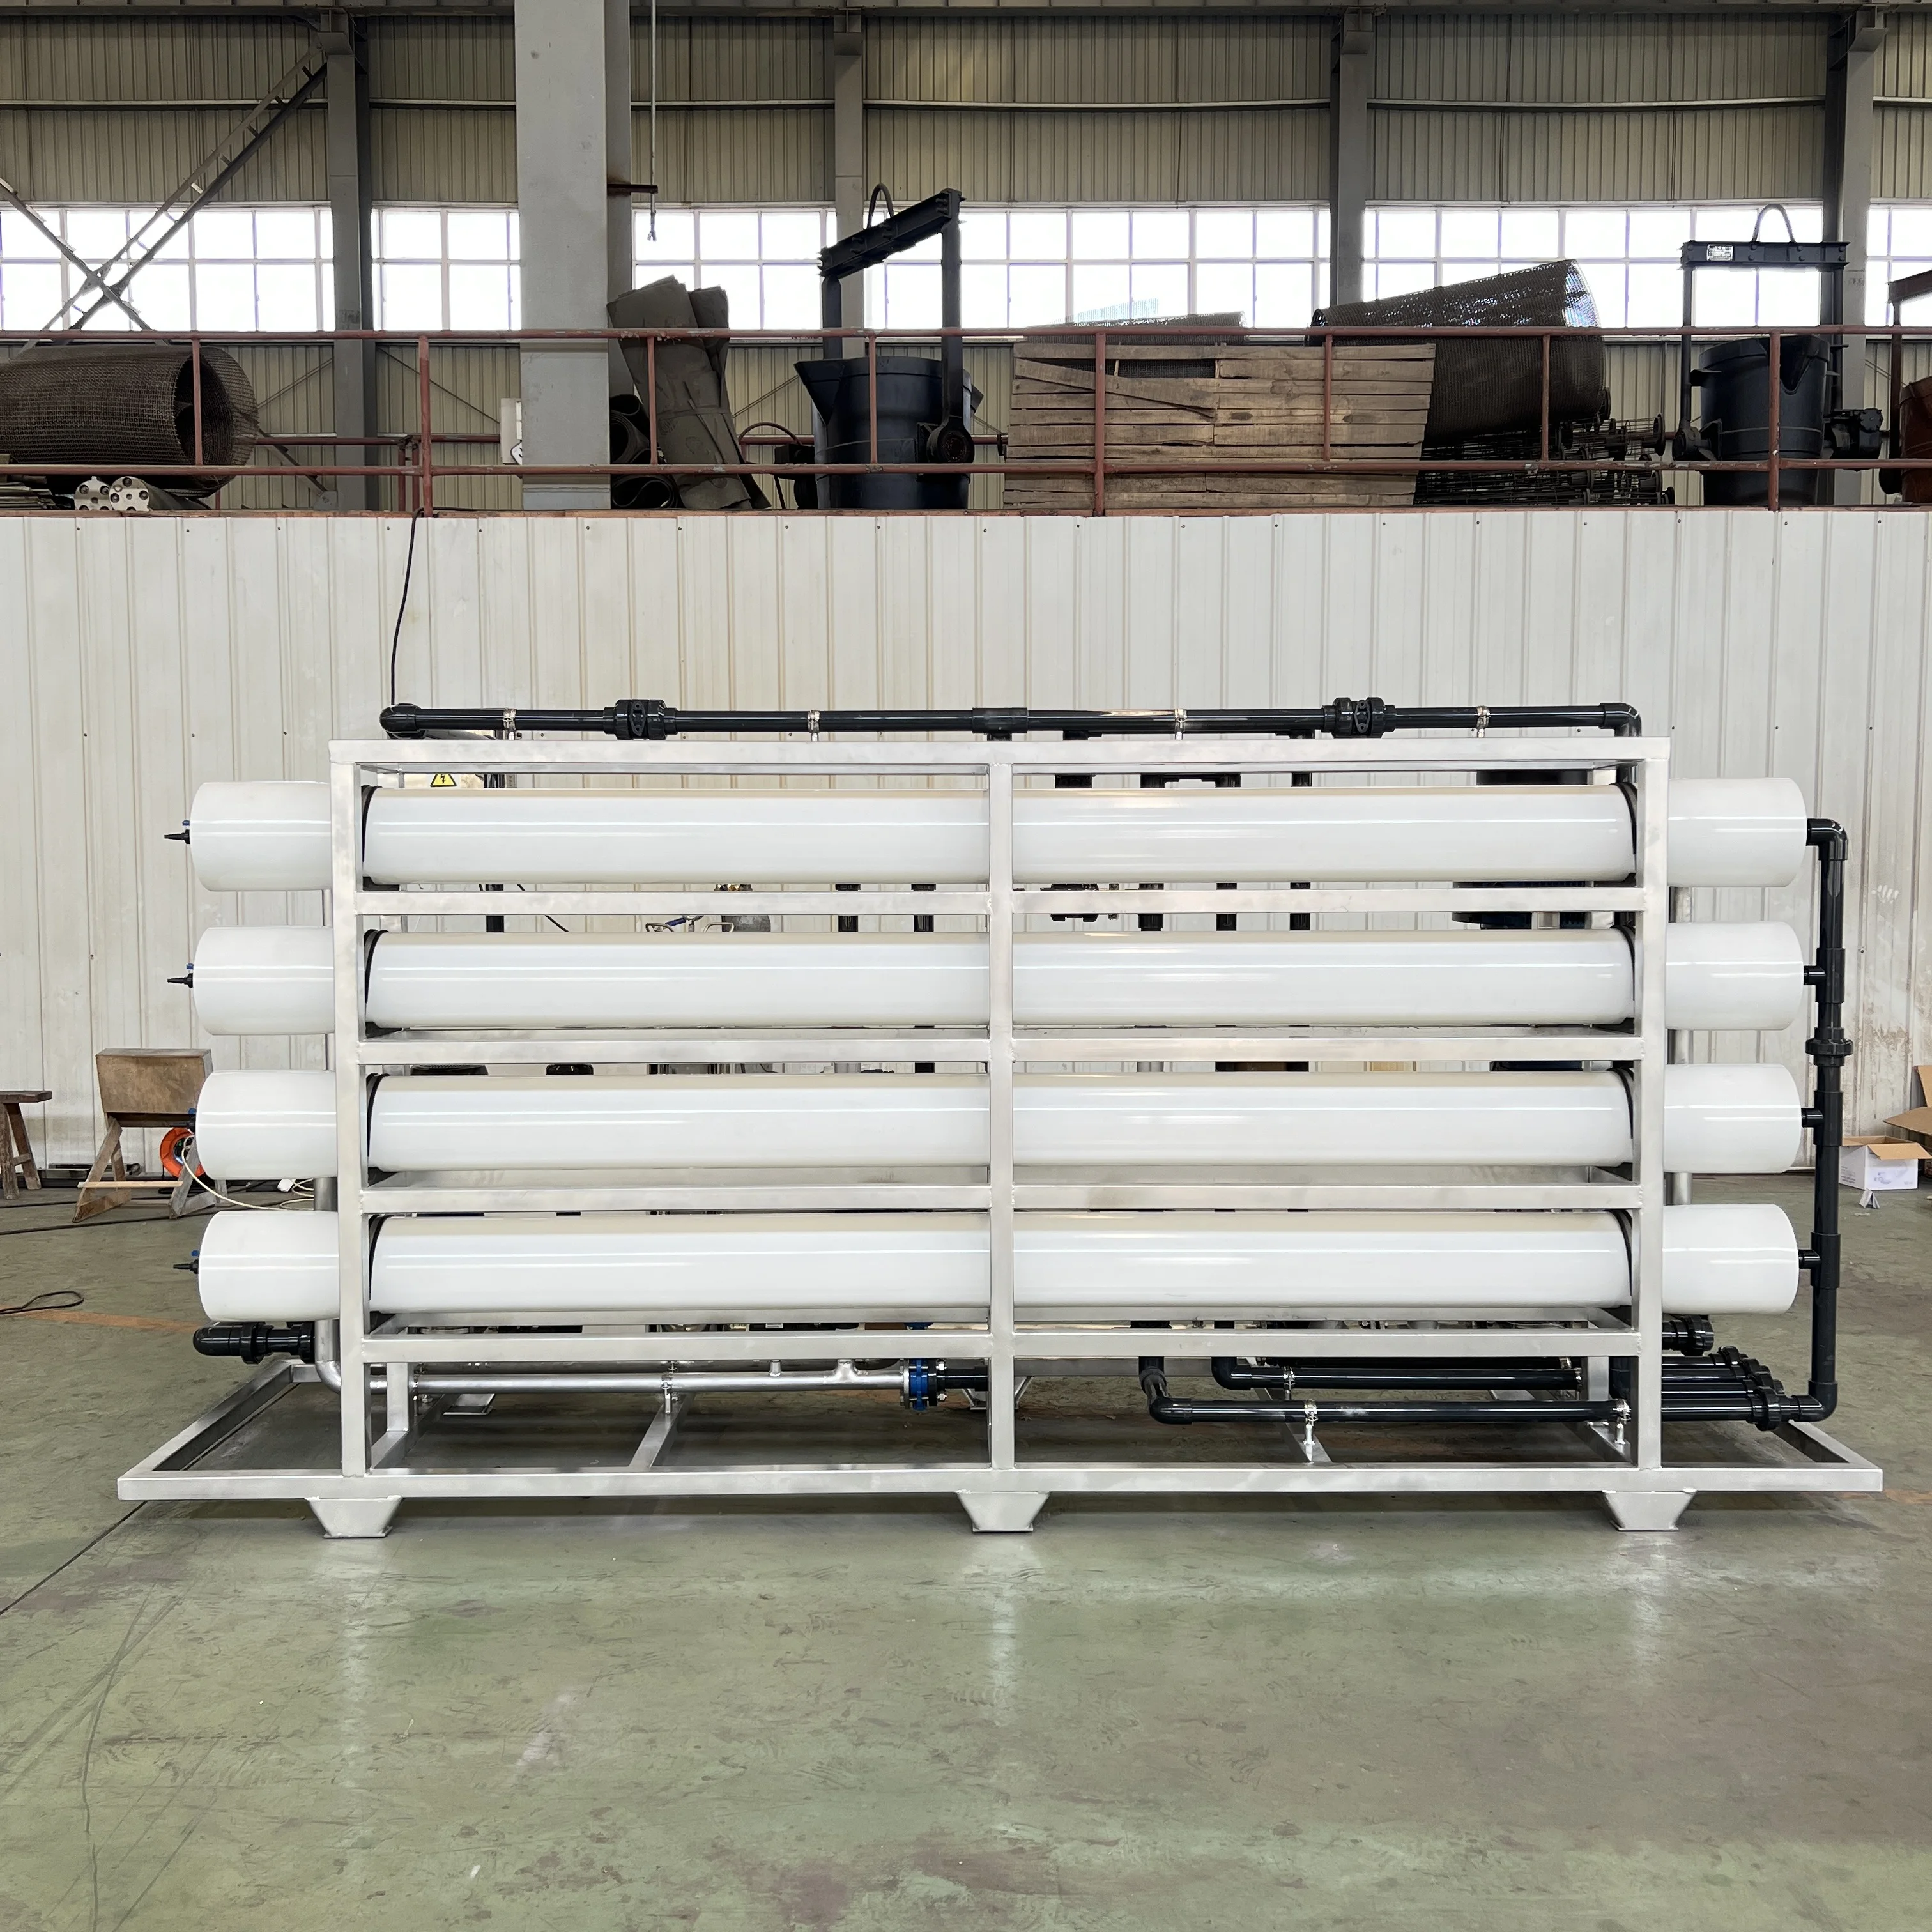
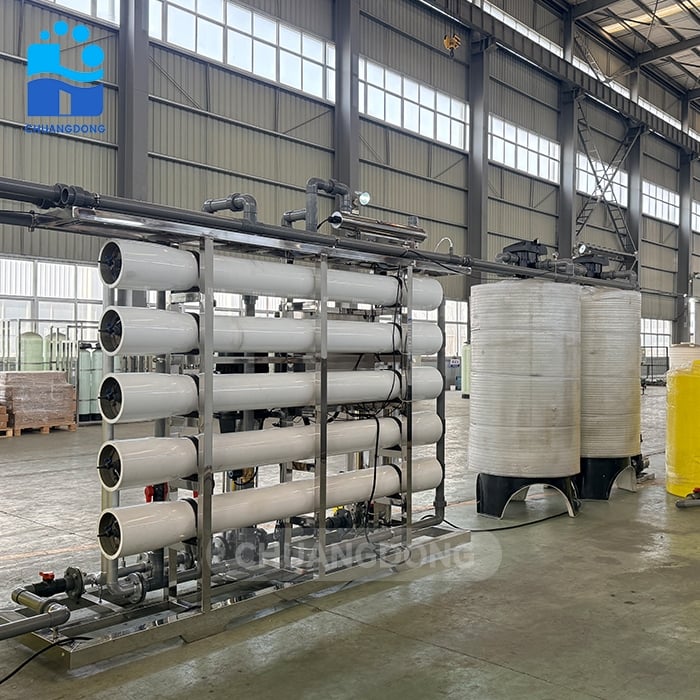
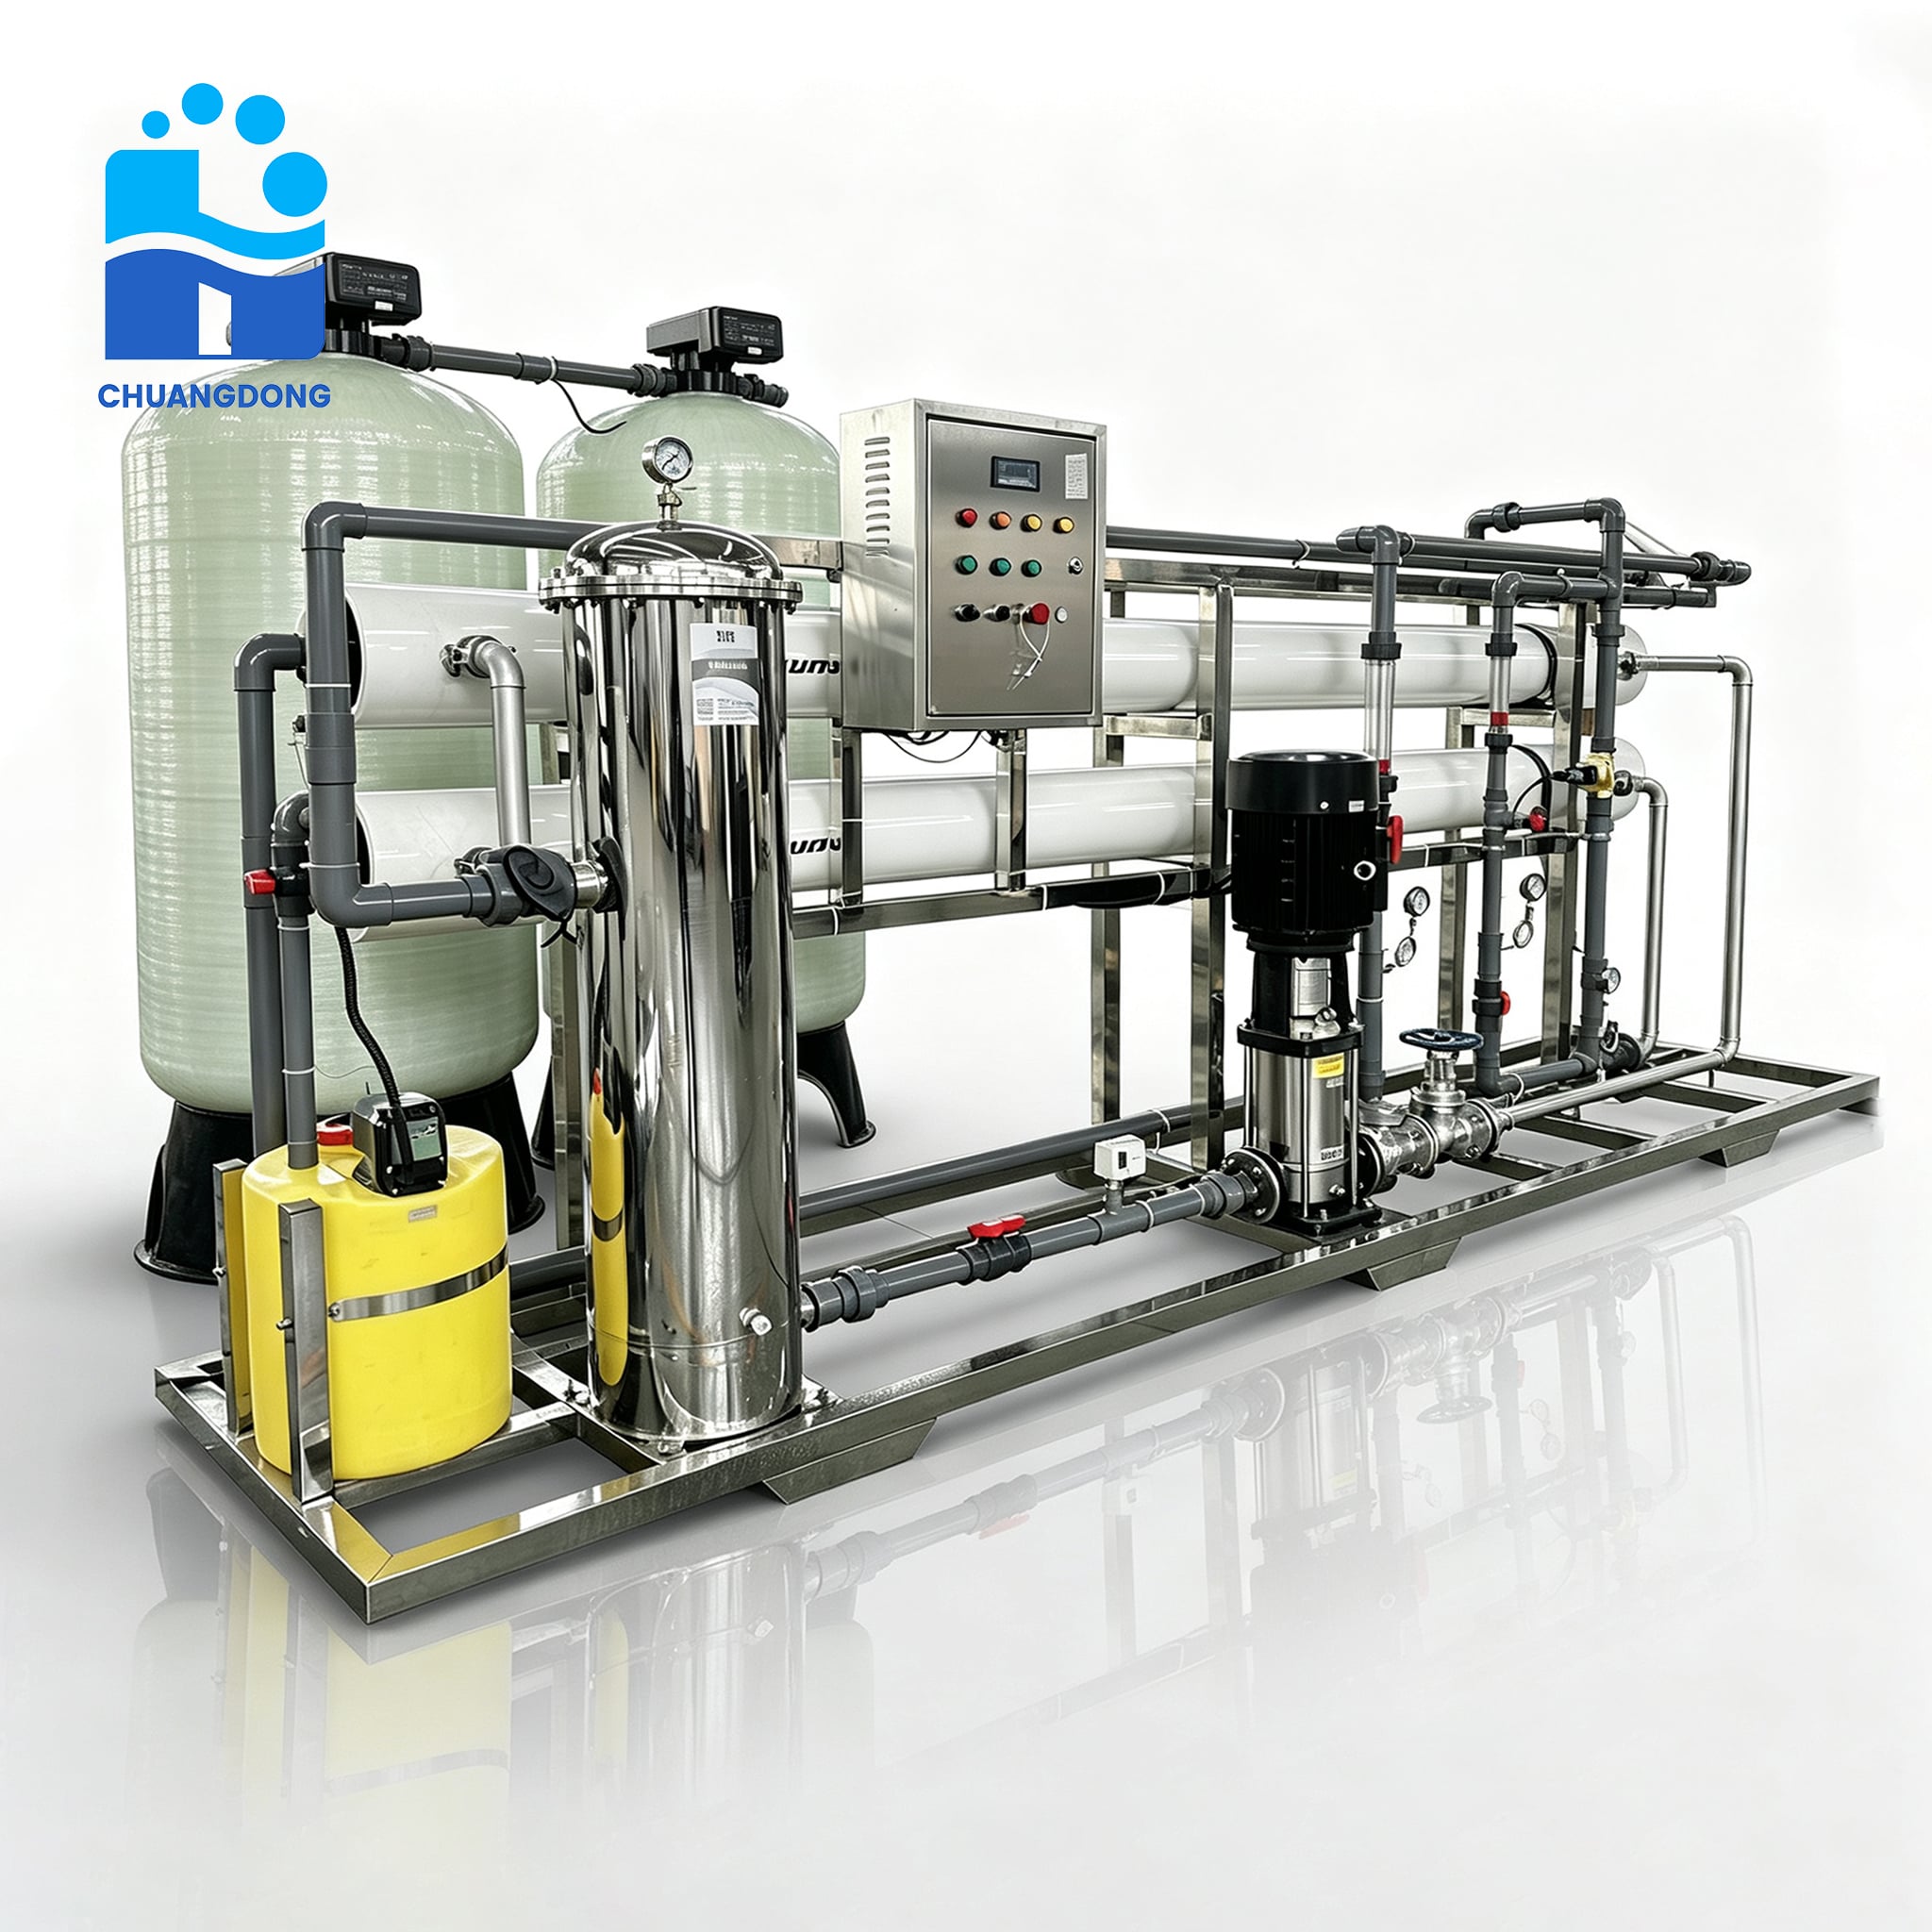
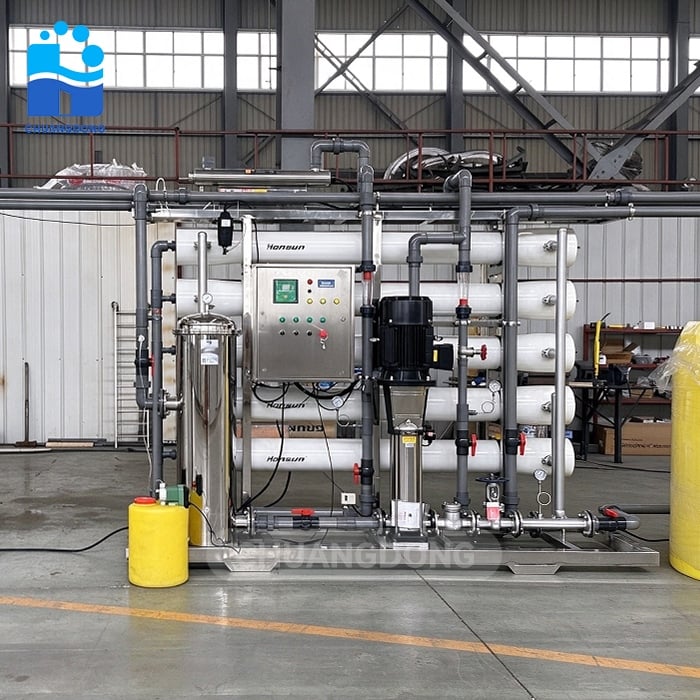
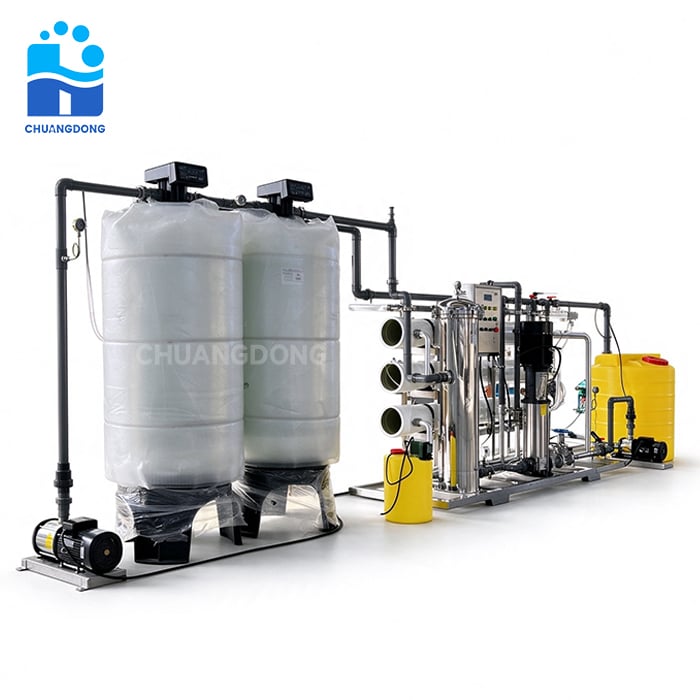
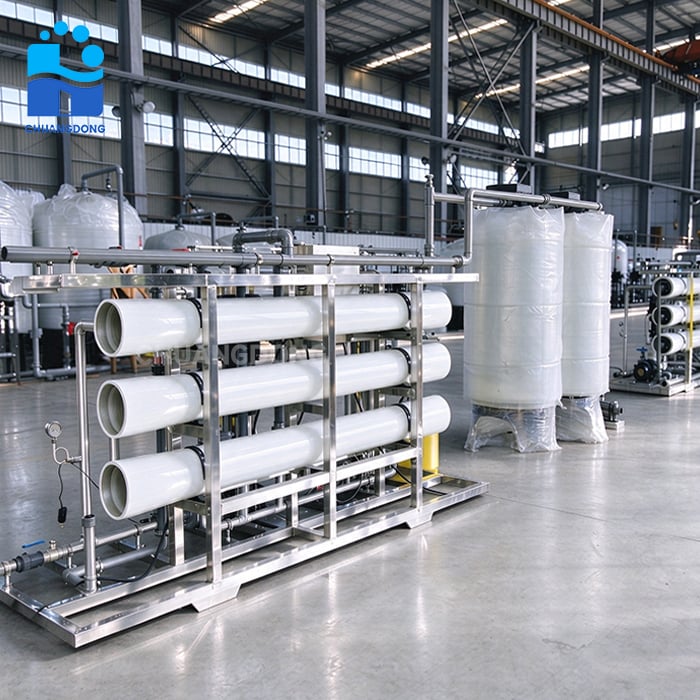
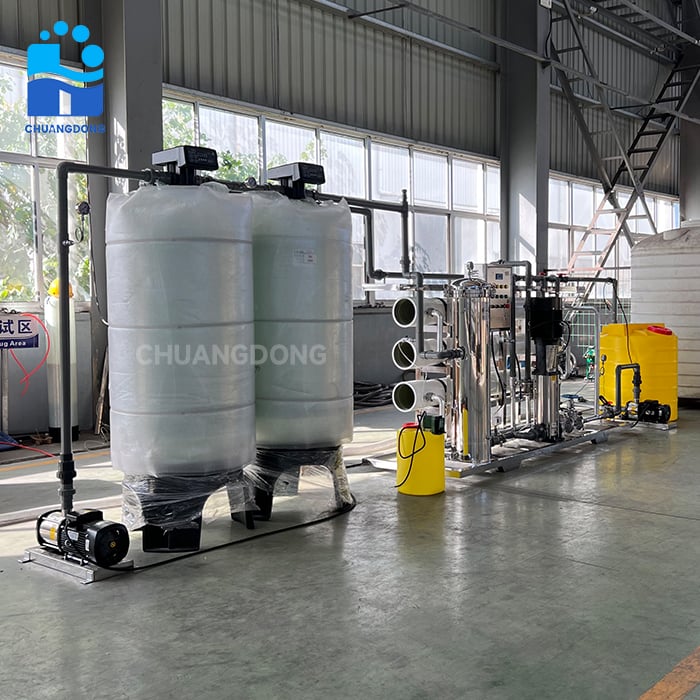
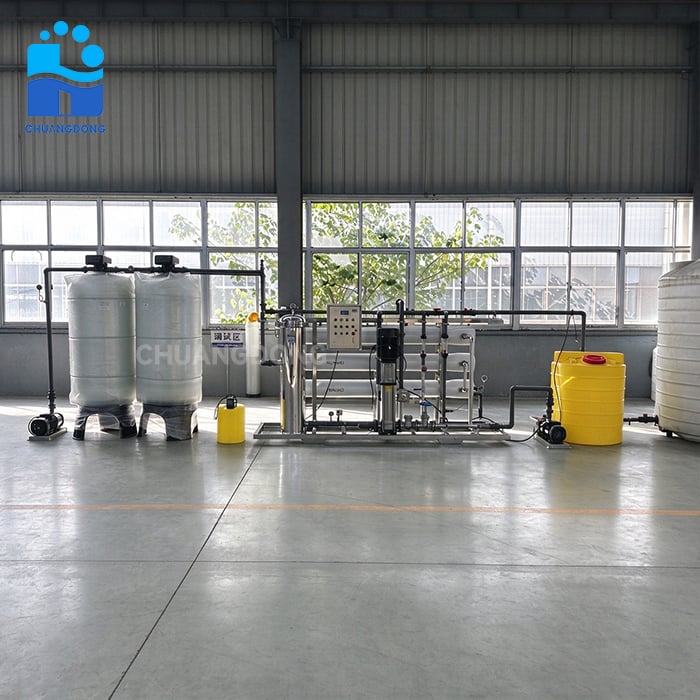
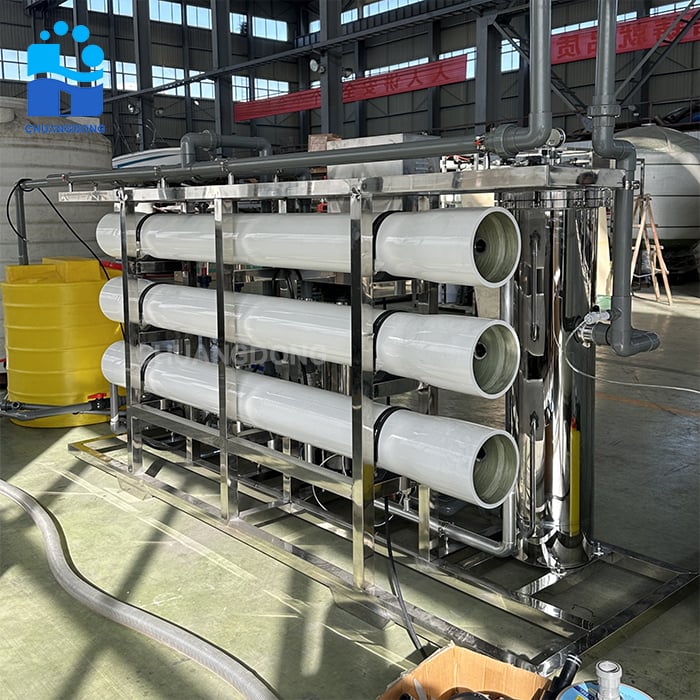
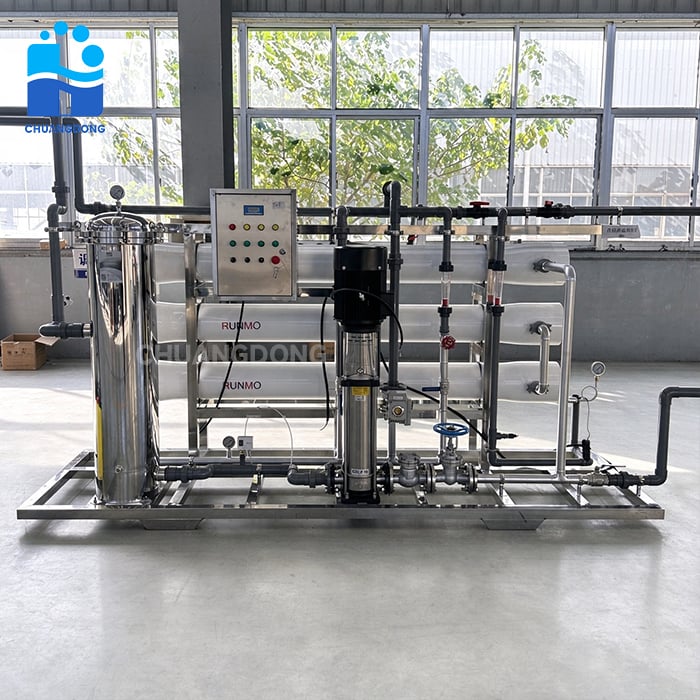
Chuangdong RO reverse osmosis systems feature a modular design with customizable treatment capacities to meet different water demands. From small-scale pilot applications and individual workshops to centralized water supply for entire production facilities, we provide flexible reverse osmosis water treatment solutions.
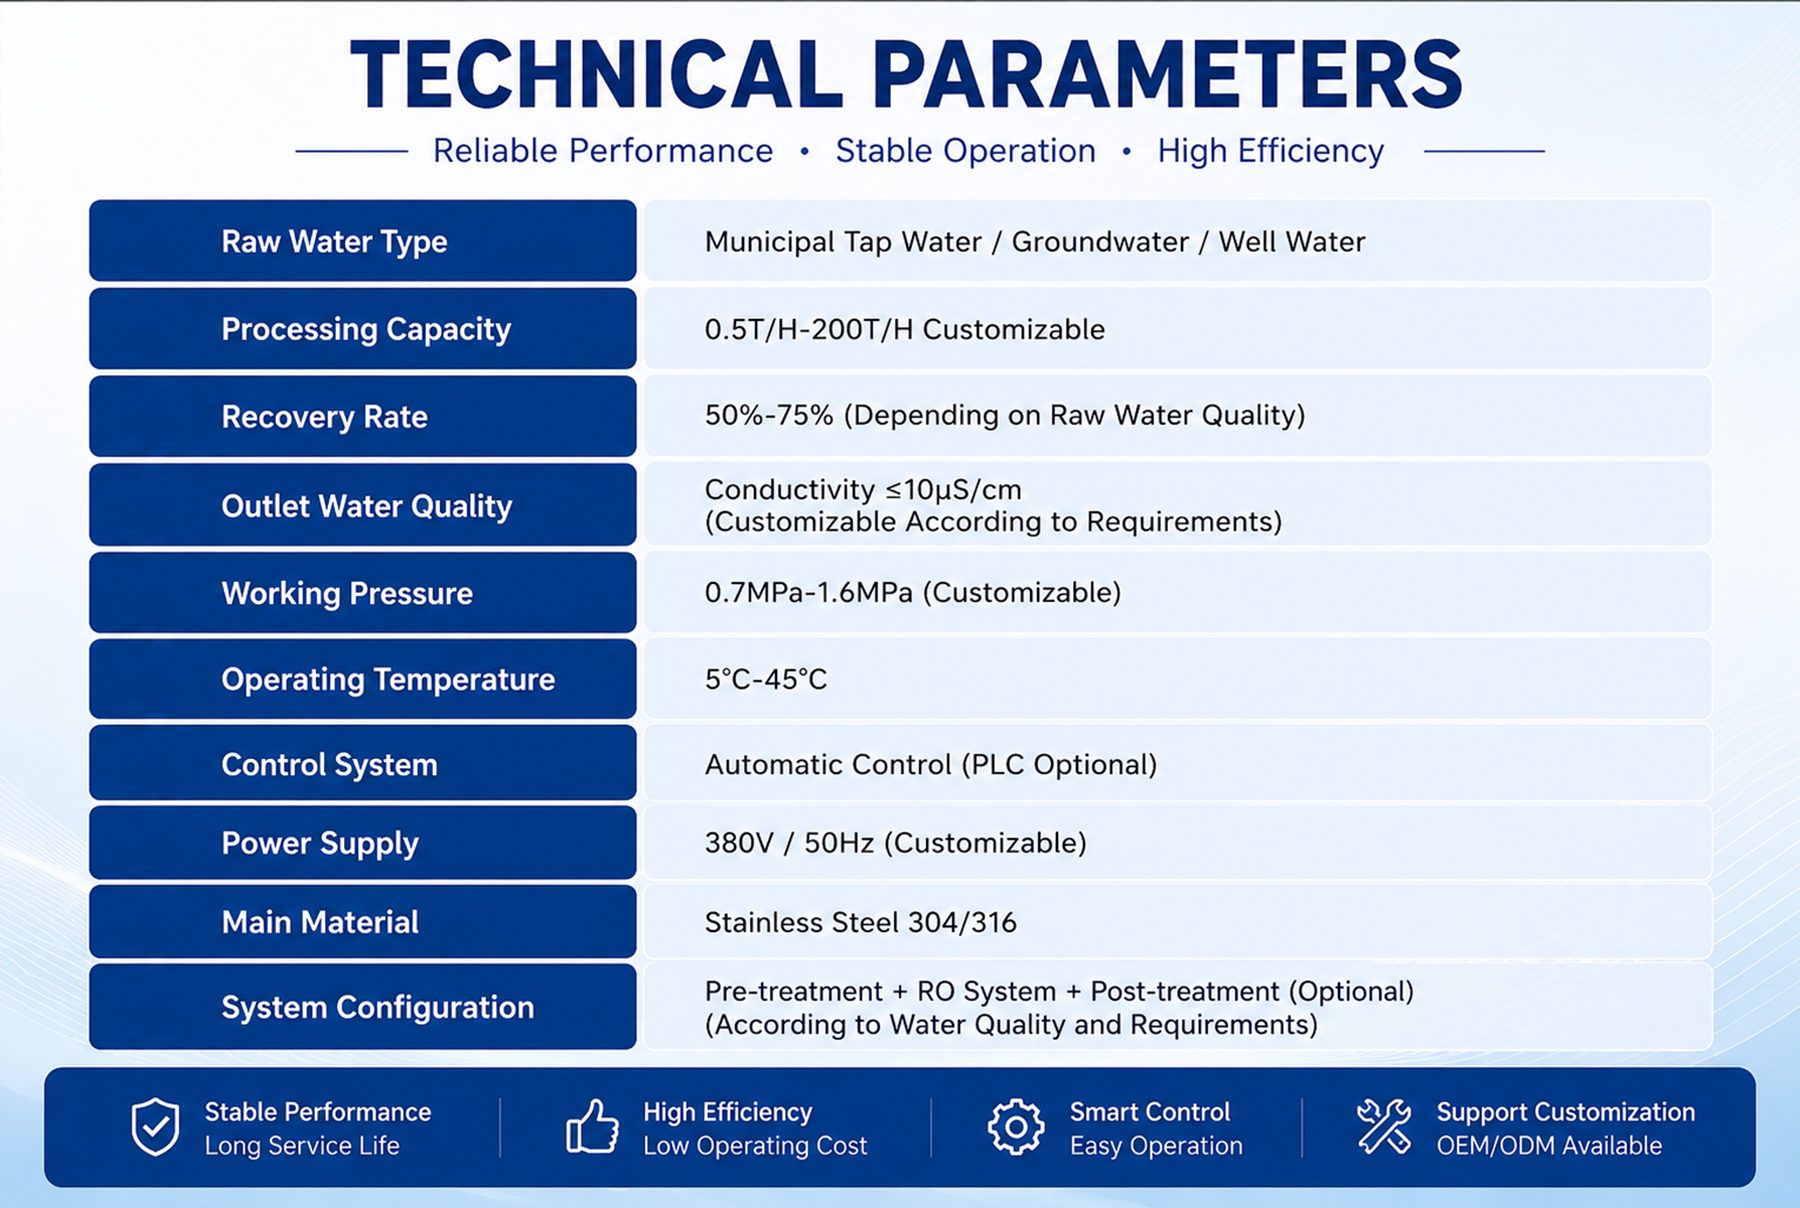
Small-Capacity Models: 0.25 t/h, 0.5 t/h, 1 t/h, and 2 t/h. Suitable for laboratories, small food processing workshops, beverage sampling, and small-scale ingredient preparation.
Standard Industrial Models: 3 t/h, 5 t/h, 10 t/h, 15 t/h, and 20 t/h. These are commonly used in food processing plants for ingredient preparation and equipment cleaning water.
Large-Scale Integrated Systems: 30 t/h, 50 t/h, 80 t/h, 100 t/h, and above. Equipped with multiple membrane modules operating in parallel, these systems are suitable for large beverage factories, dairy plants, and pre-packaged food processing facilities.
The actual permeate output depends on factors such as inlet water temperature, TDS, and operating pressure. During the initial design stage, the membrane configuration and water recovery rate are determined based on the raw water quality to ensure the RO water treatment system meets the required operating conditions.
Key Features of Reverse Osmosis Systems
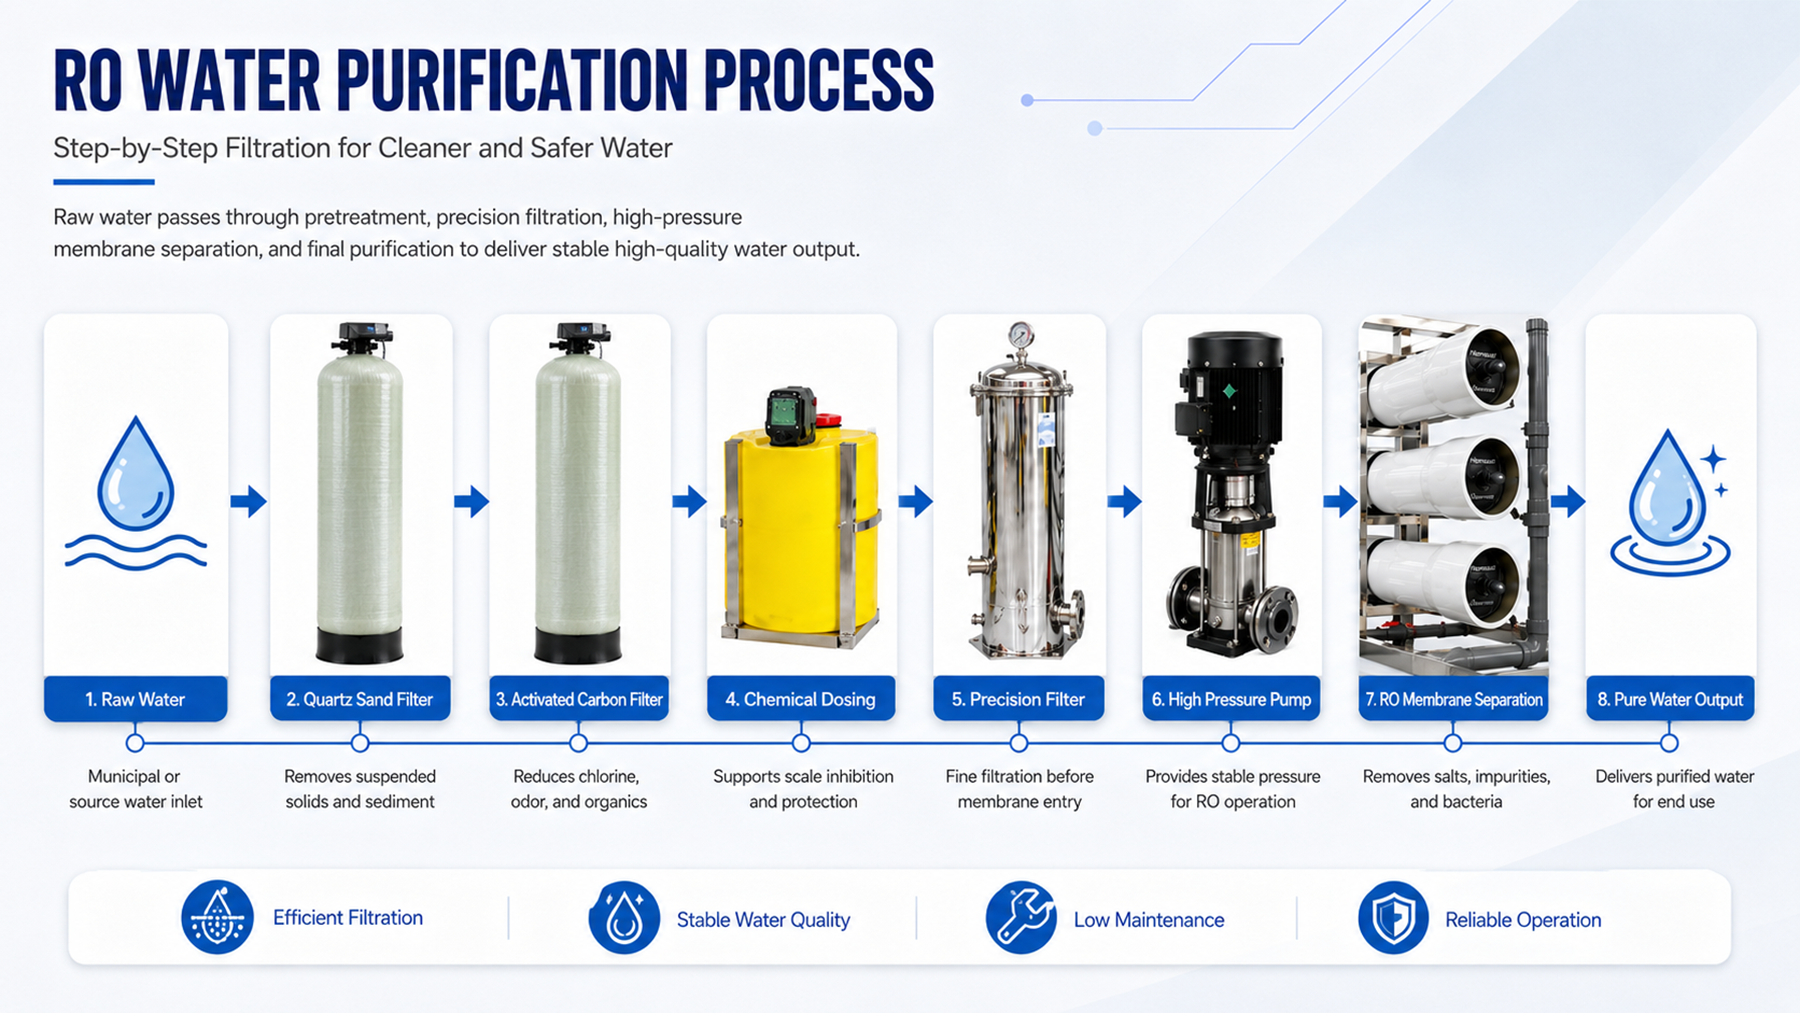
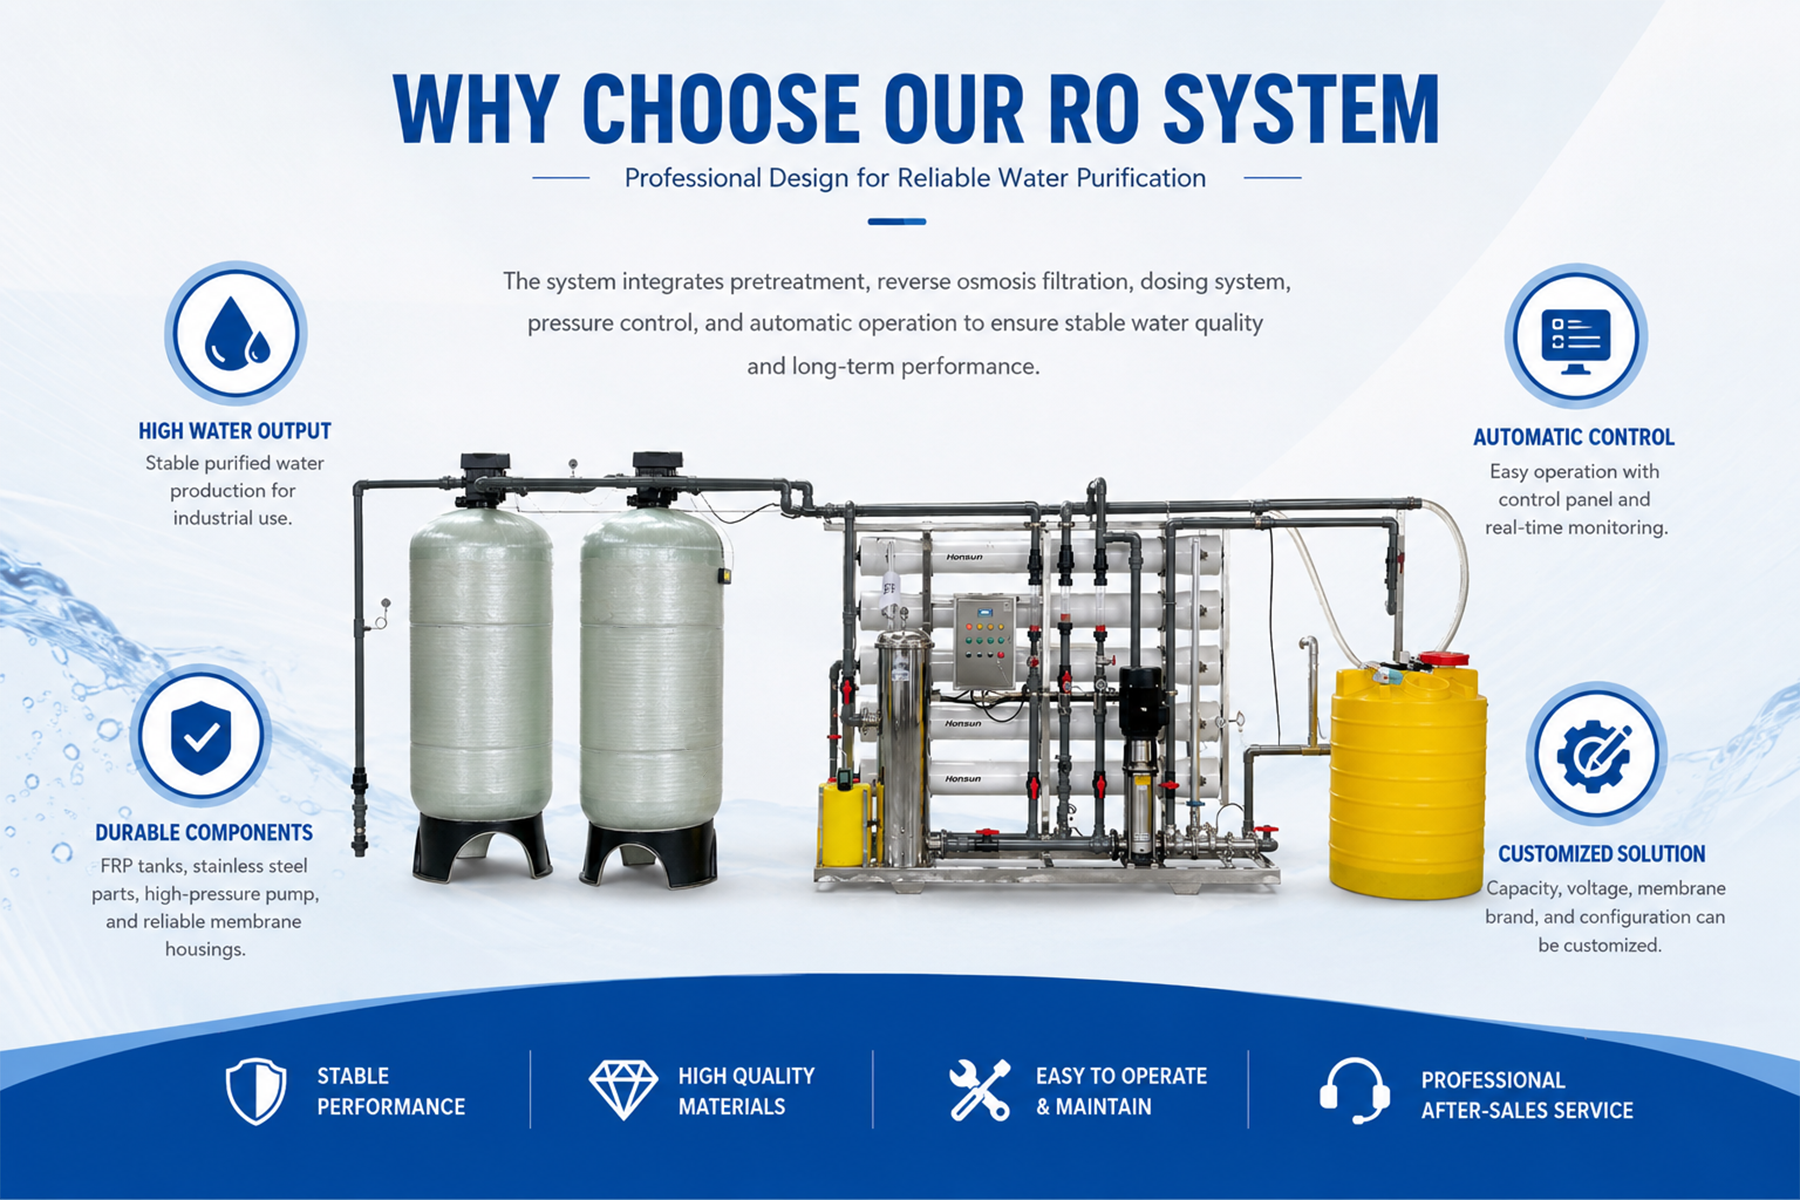
RO membranes effectively remove heavy metals, dissolved salts, colloids, bacteria, and other impurities, achieving a stable desalination rate of ≥98% to ensure consistently high-quality purified water.
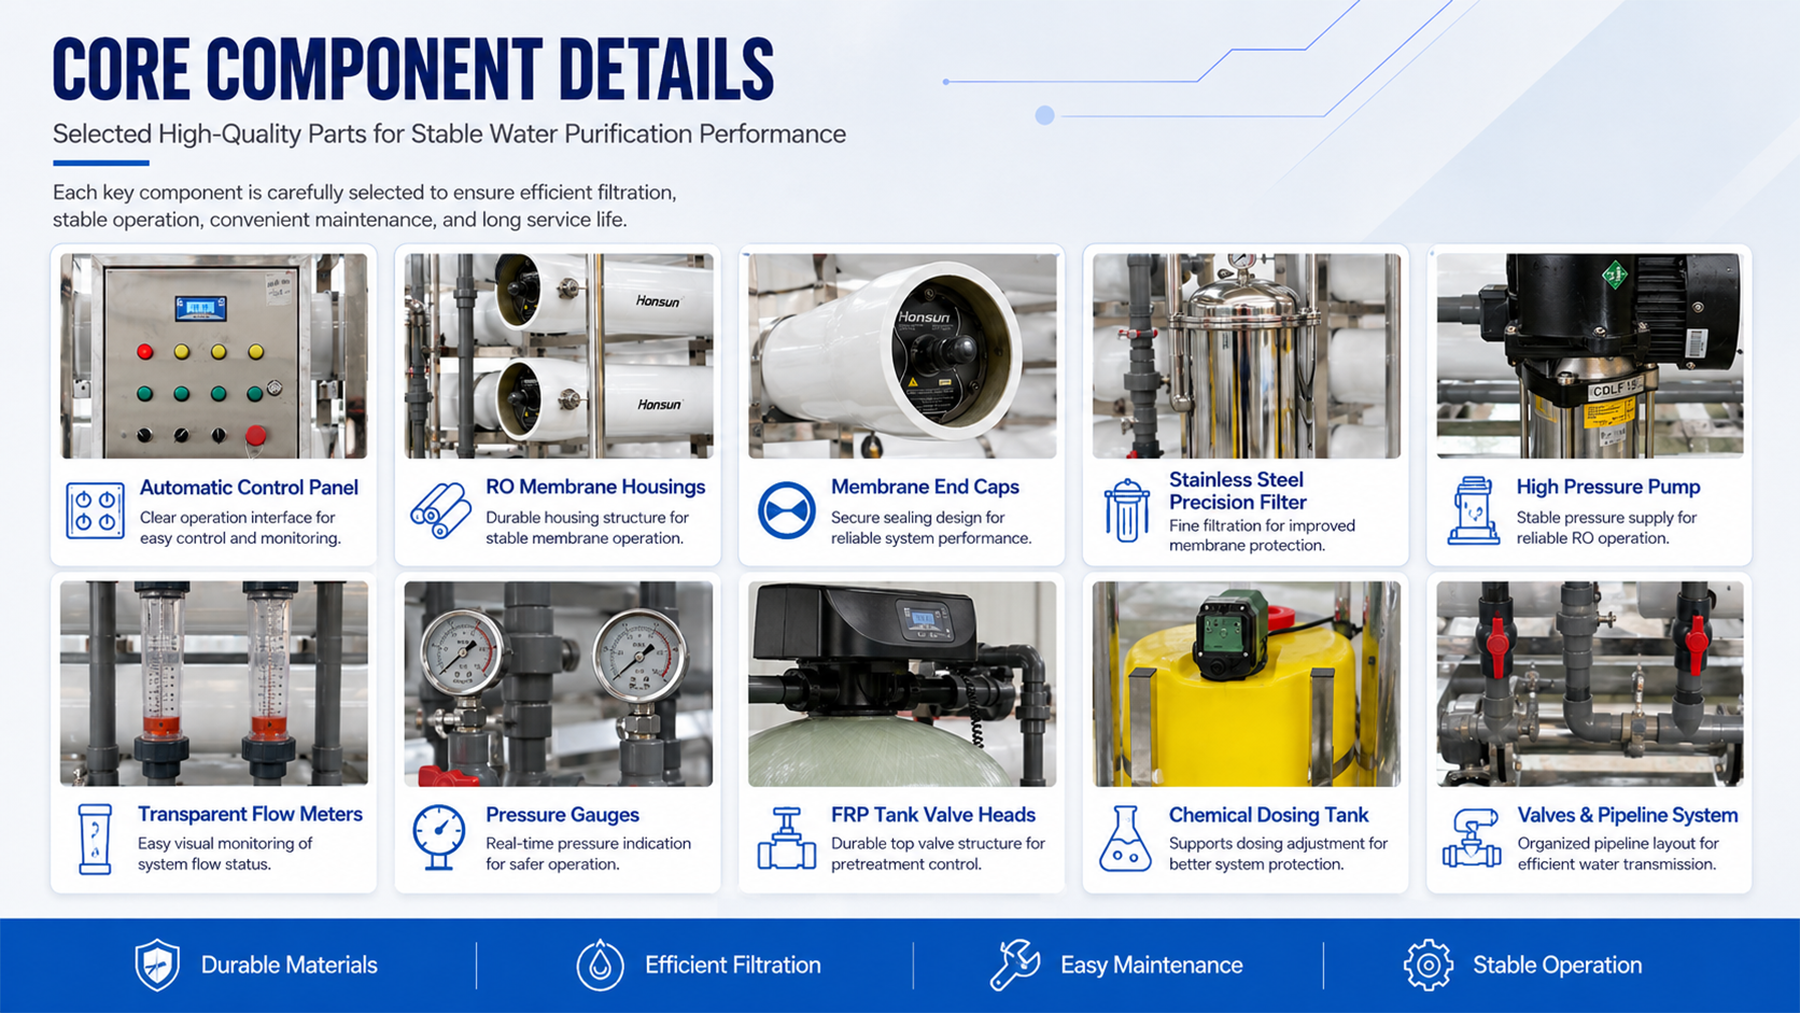
All water-contact components, including pipes, membrane housings, and water storage tanks, are made of 304 or 316L stainless steel. The system supports regular CIP (Clean-in-Place) cleaning, helping prevent material leaching and secondary contamination while meeting food hygiene requirements.
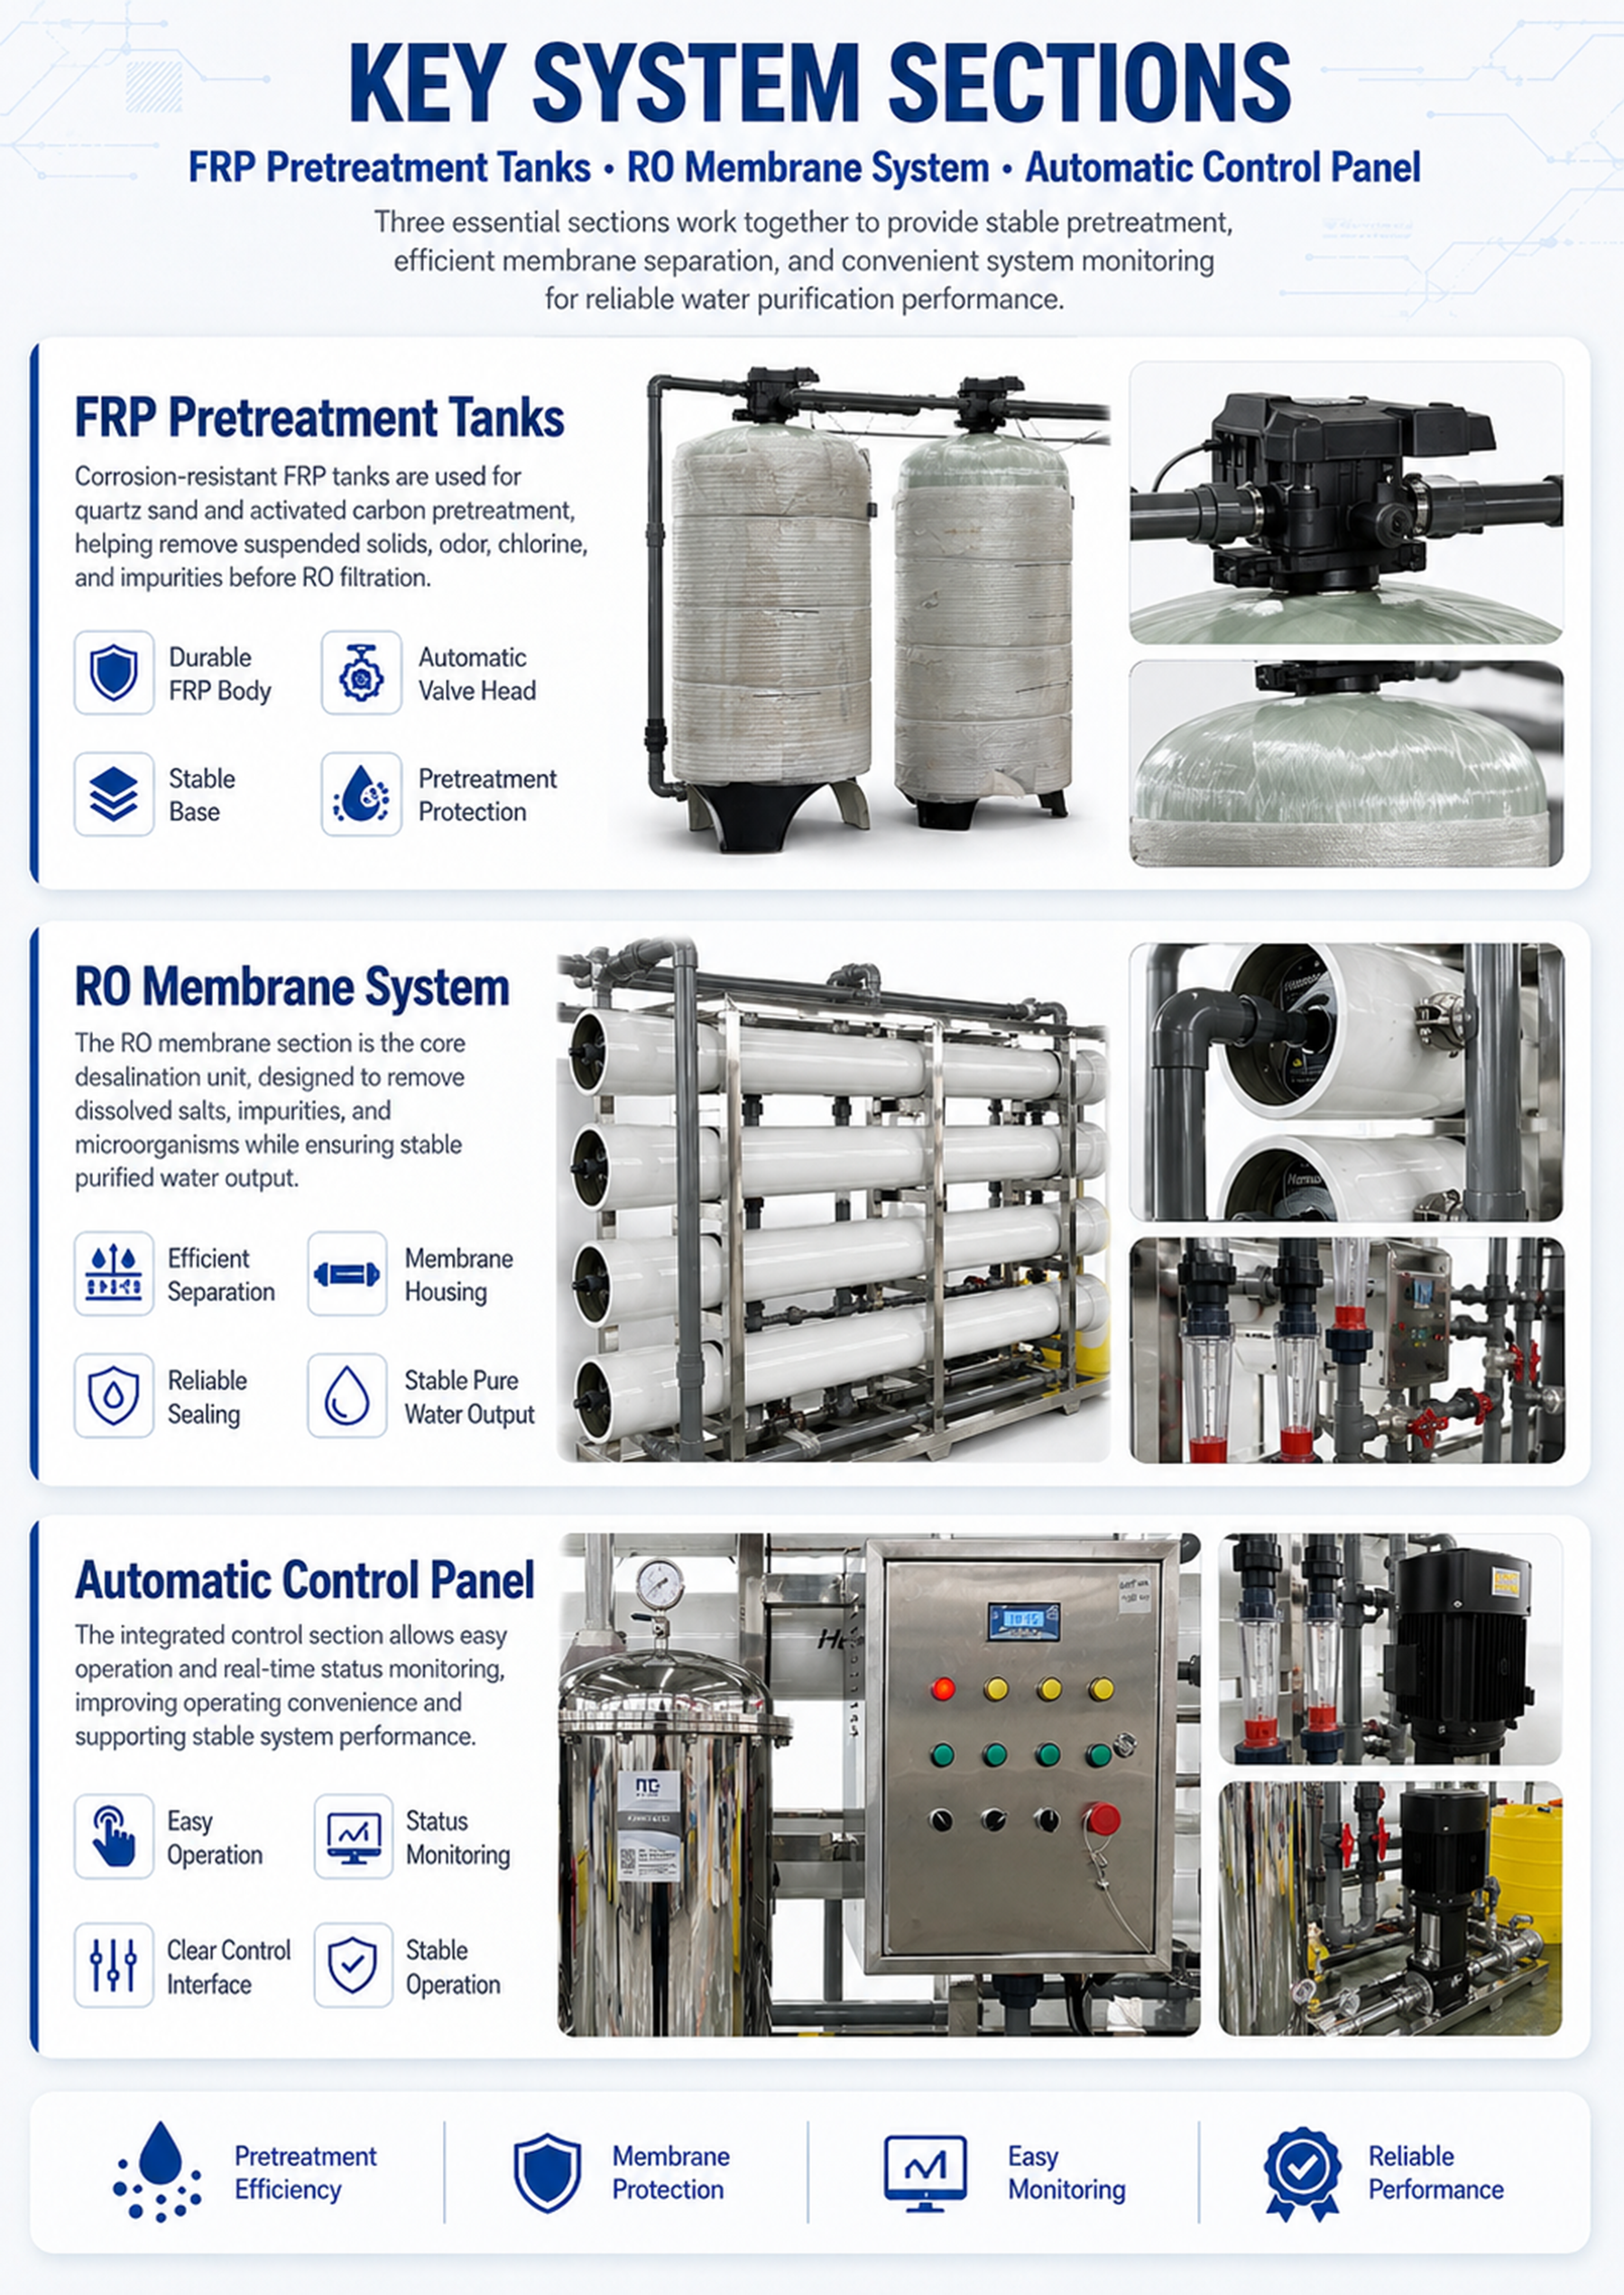
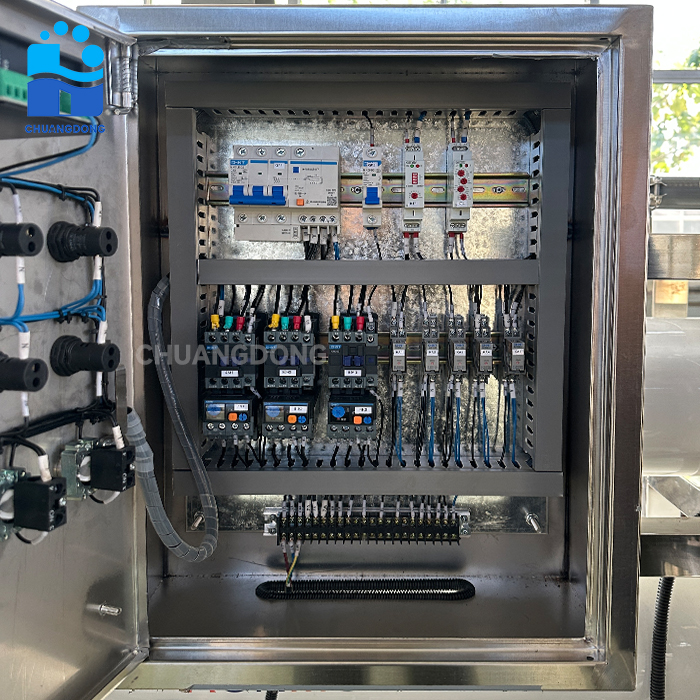
Equipped with an intelligent PLC control system, the RO water treatment system provides real-time monitoring of water quality, flow rates, and operating pressure. Its modular design allows for easy capacity expansion when needed, while requiring minimal installation space.
Chuangdong's Project Experience
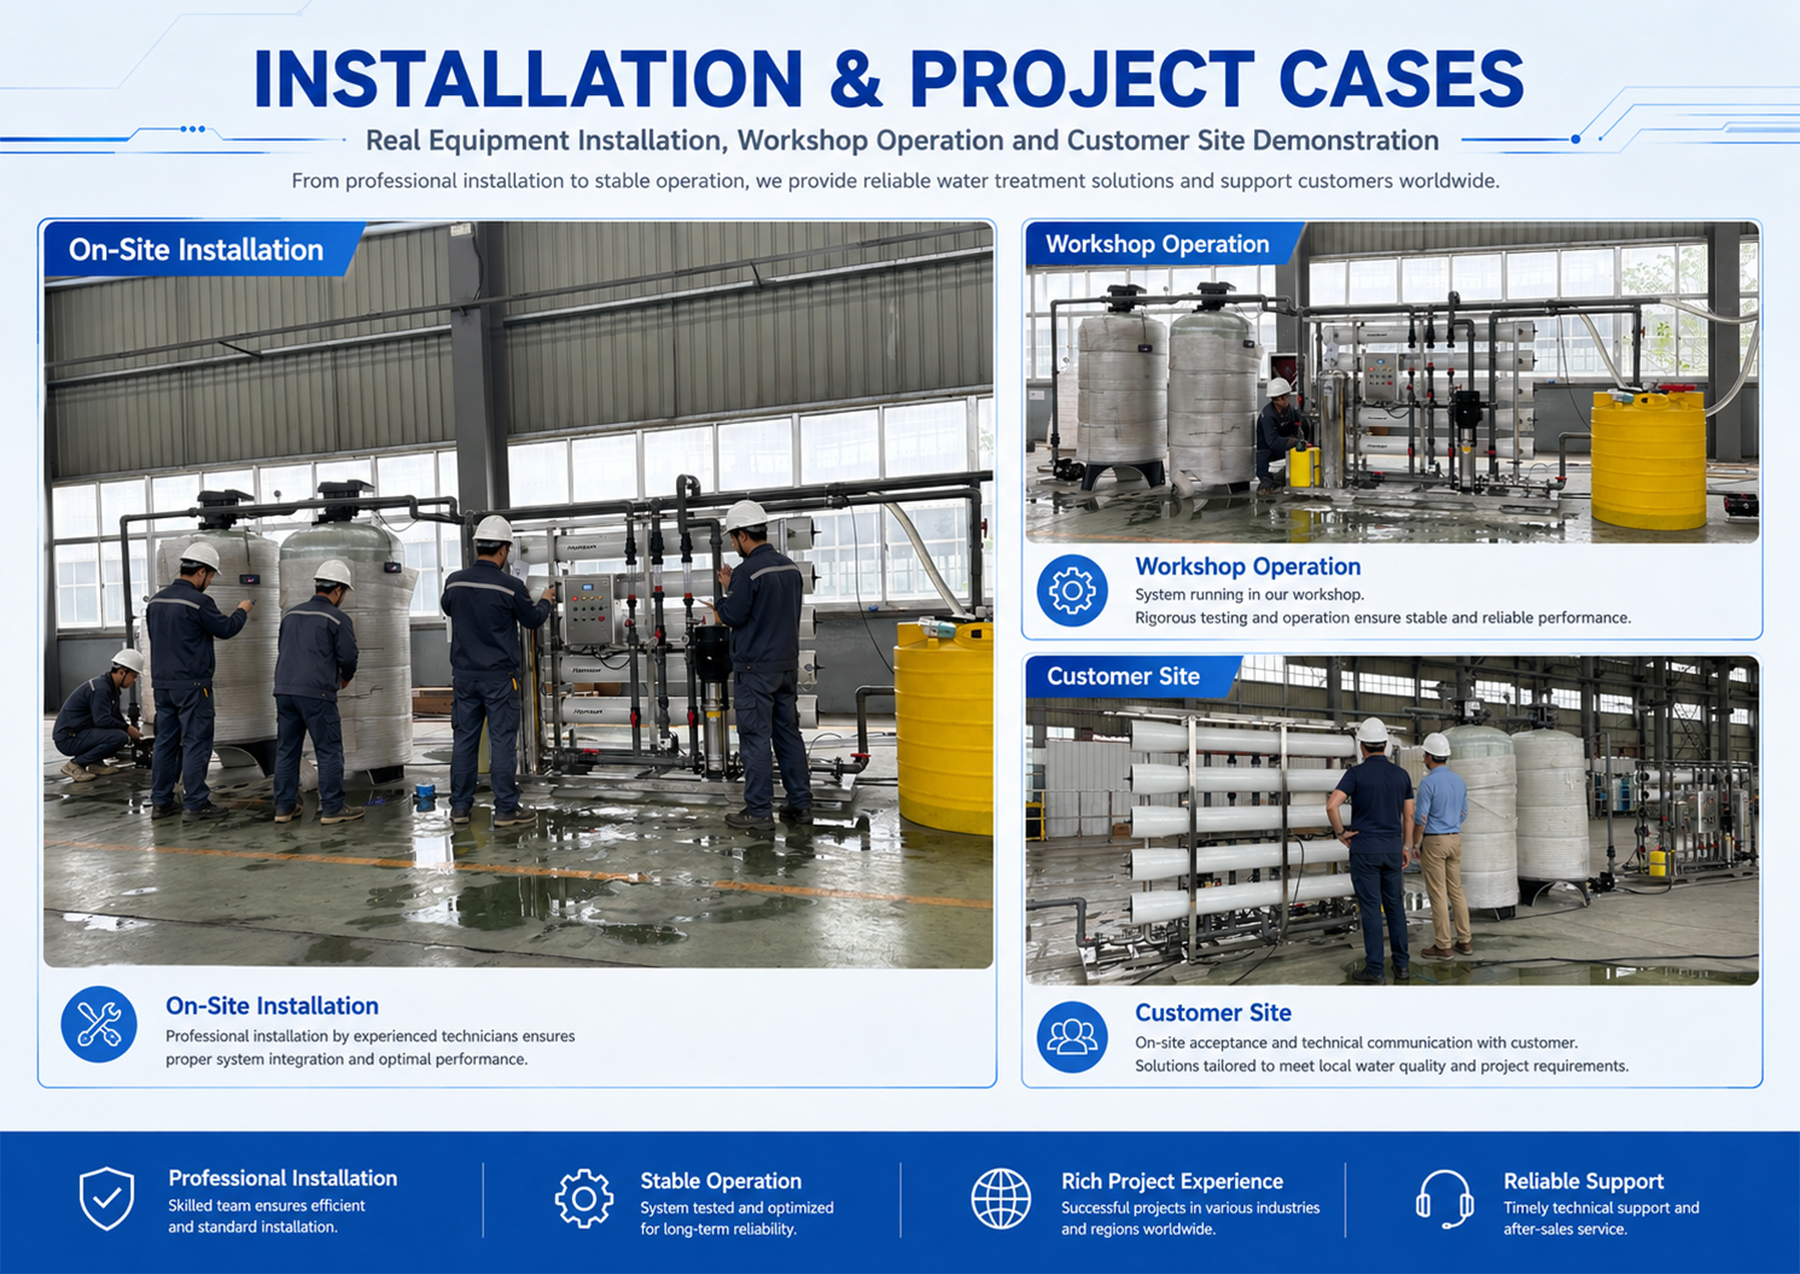
Chuangdong has extensive experience in designing and delivering industrial pure water treatment systems, with a proven track record across various international projects. We understand the differences in local water quality and food industry regulations across different countries. Our representative overseas food processing water treatment projects include:
Thailand: 6 t/h Two-Pass RO Water Treatment System for Milk Powder Production
The project uses groundwater with high hardness and nitrate levels as its raw water source. The entire system features 316L sanitary-grade stainless steel piping. The complete solution includes pretreatment, two-pass reverse osmosis, UV sterilization, and a hygienic water supply system, along with on-site installation and commissioning and operator training. The system is designed to meet the hygiene requirements of Thai food processing facilities and support food safety audits.
Nigeria: 15 t/h RO Pure Water System for a Bottled Juice Factory
The solution features a pre-filtration and ultrafiltration system combined with food-grade, anti-fouling RO membranes. Additional pressure stabilization and power failure protection modules ensure stable system operation. The treated water is used for juice blending and bottle rinsing. Its modular design simplifies on-site installation and reduces construction complexity, making it suitable for the high-temperature conditions of tropical West Africa.
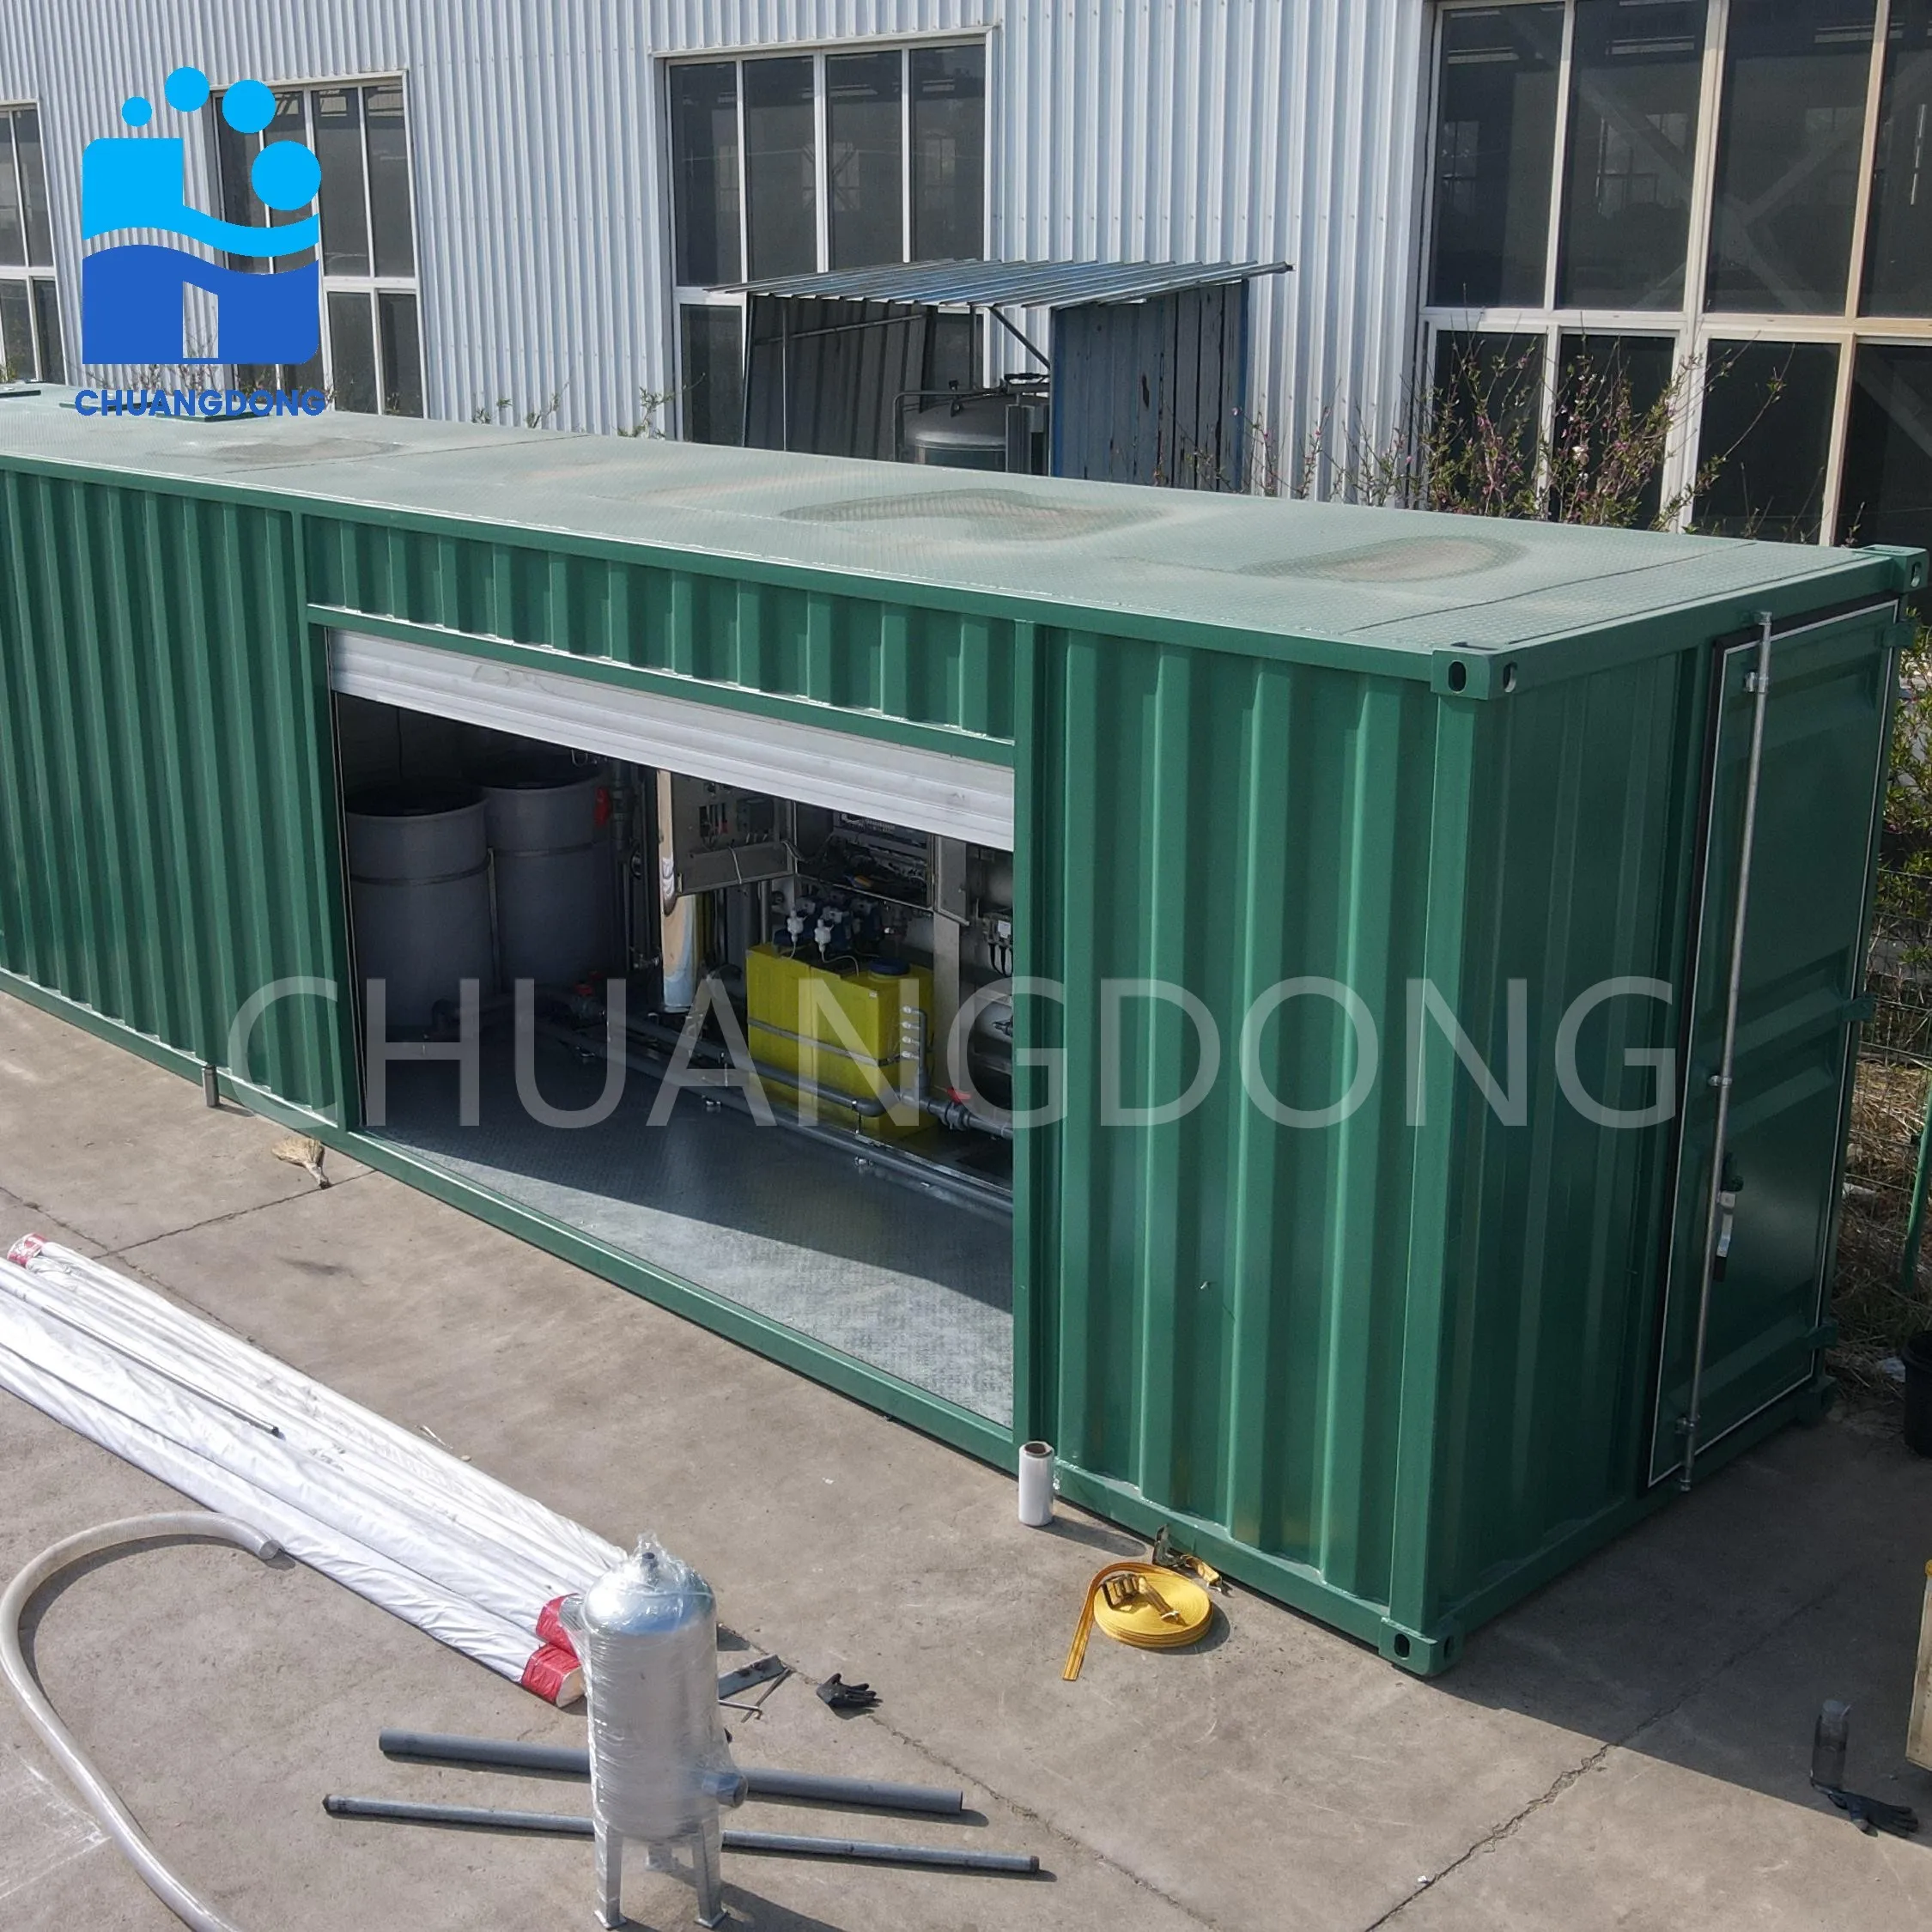
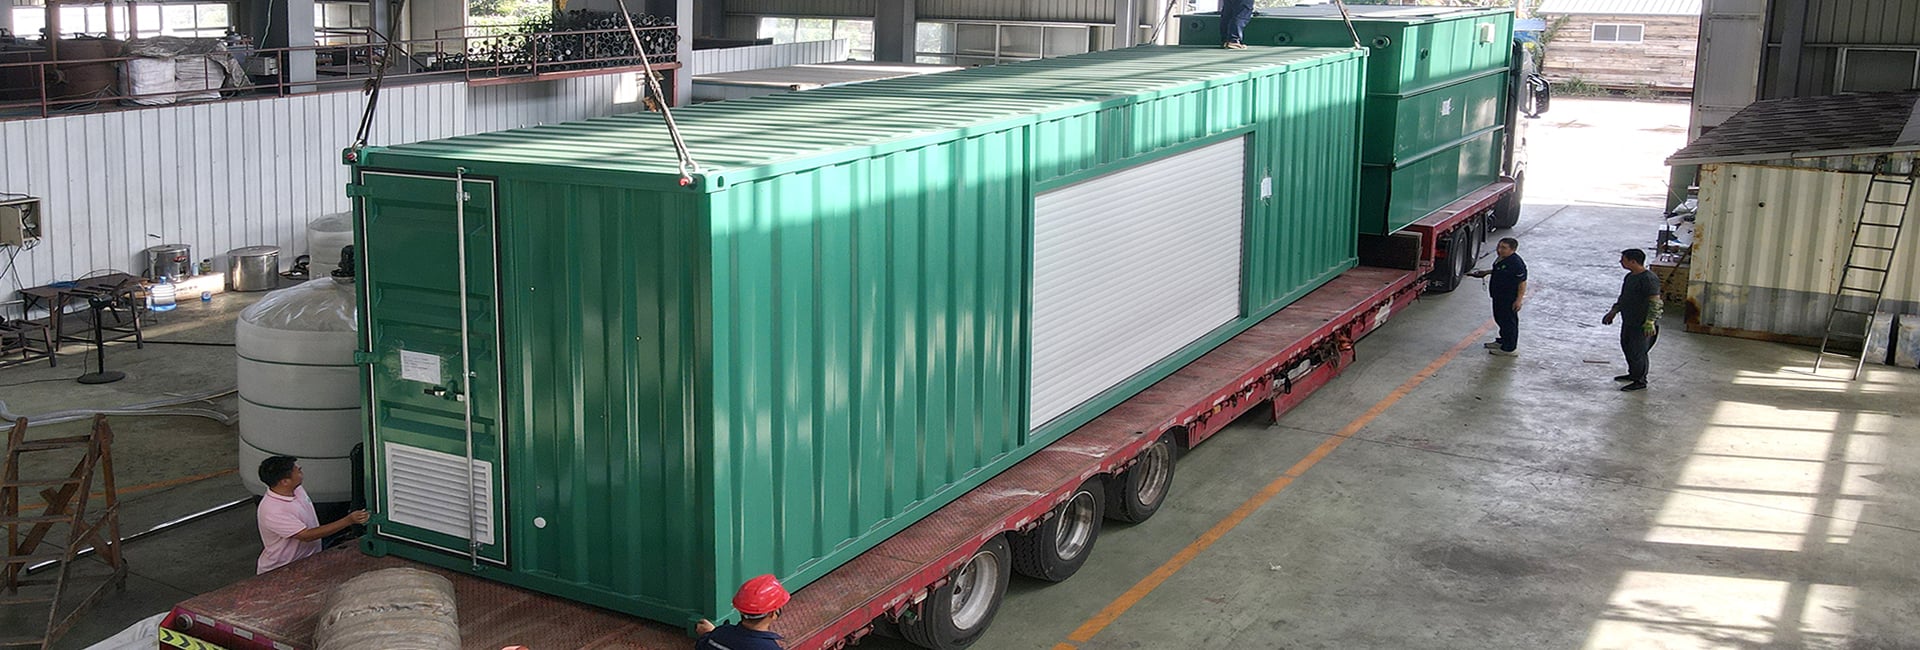
Saudi Arabia: 4 t/h Containerized RO Water Treatment System for Date Processing
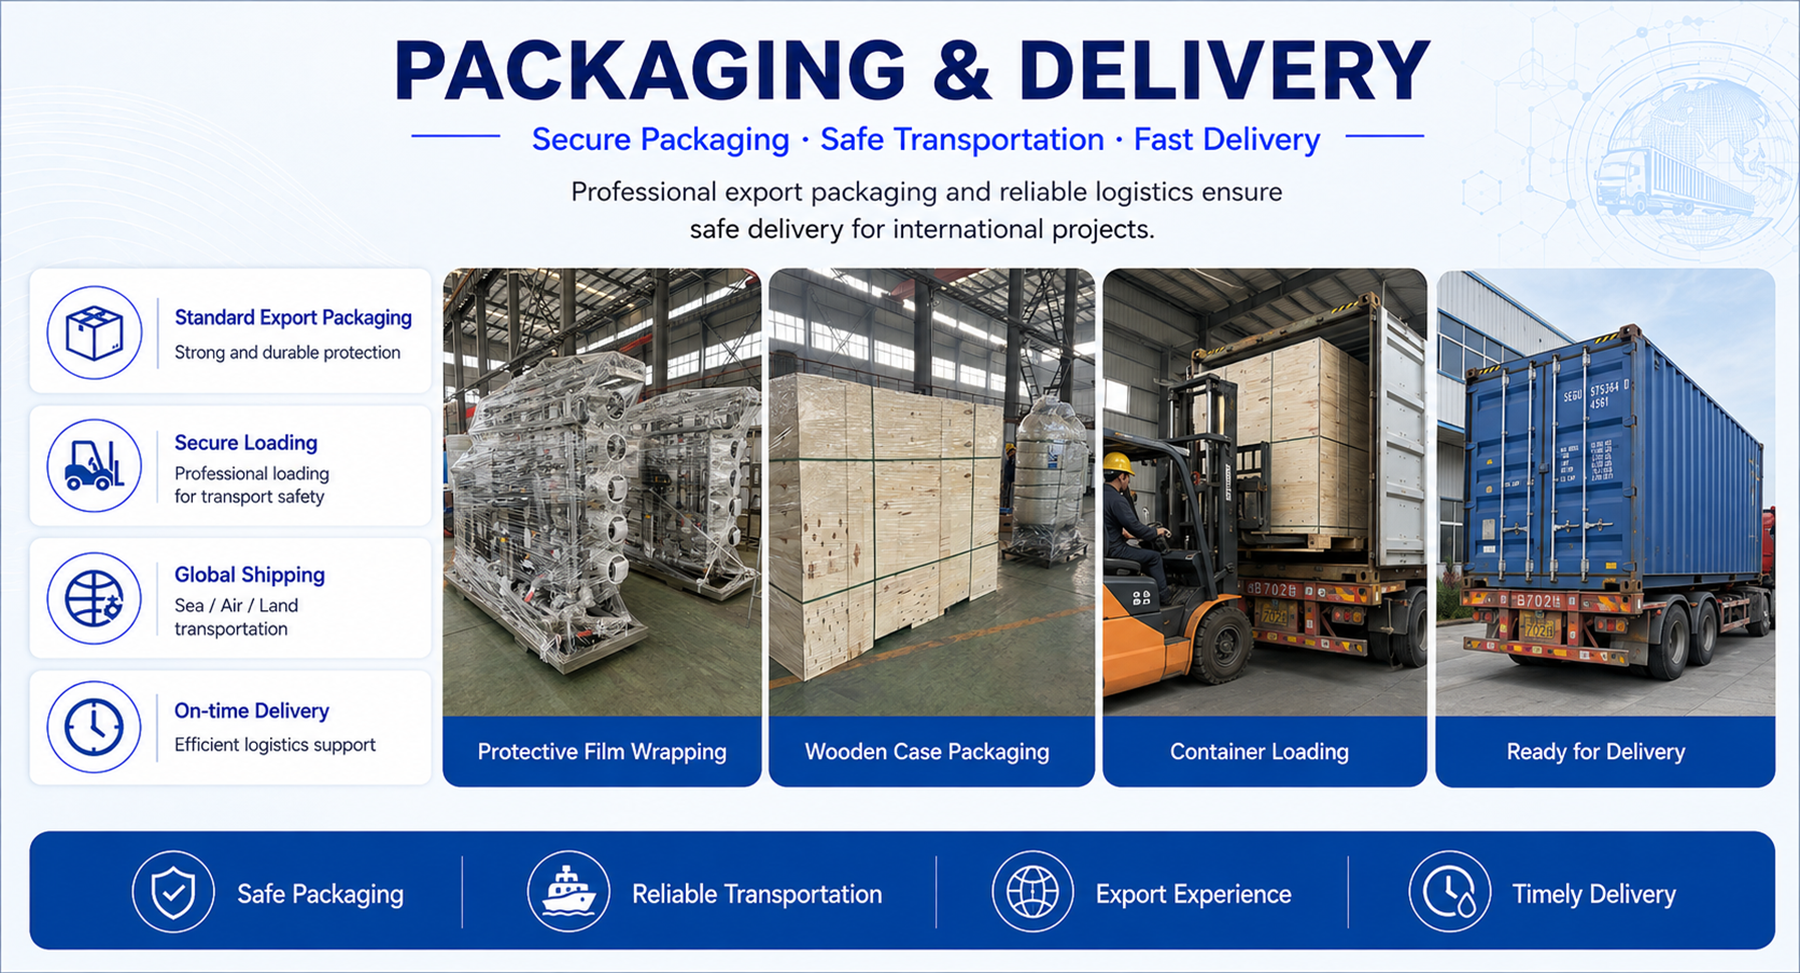
The client primarily uses the system for date cleaning and candying processes. The skid-mounted containerized RO system features a compact design and requires minimal installation space. It can be quickly put into operation after connection to the water and power supplies. The system also includes a concentrate recovery unit to improve water recovery and overall water resource utilization.
View More of Our Water Treatment Project Case Studies
Applications of RO Reverse Osmosis Systems
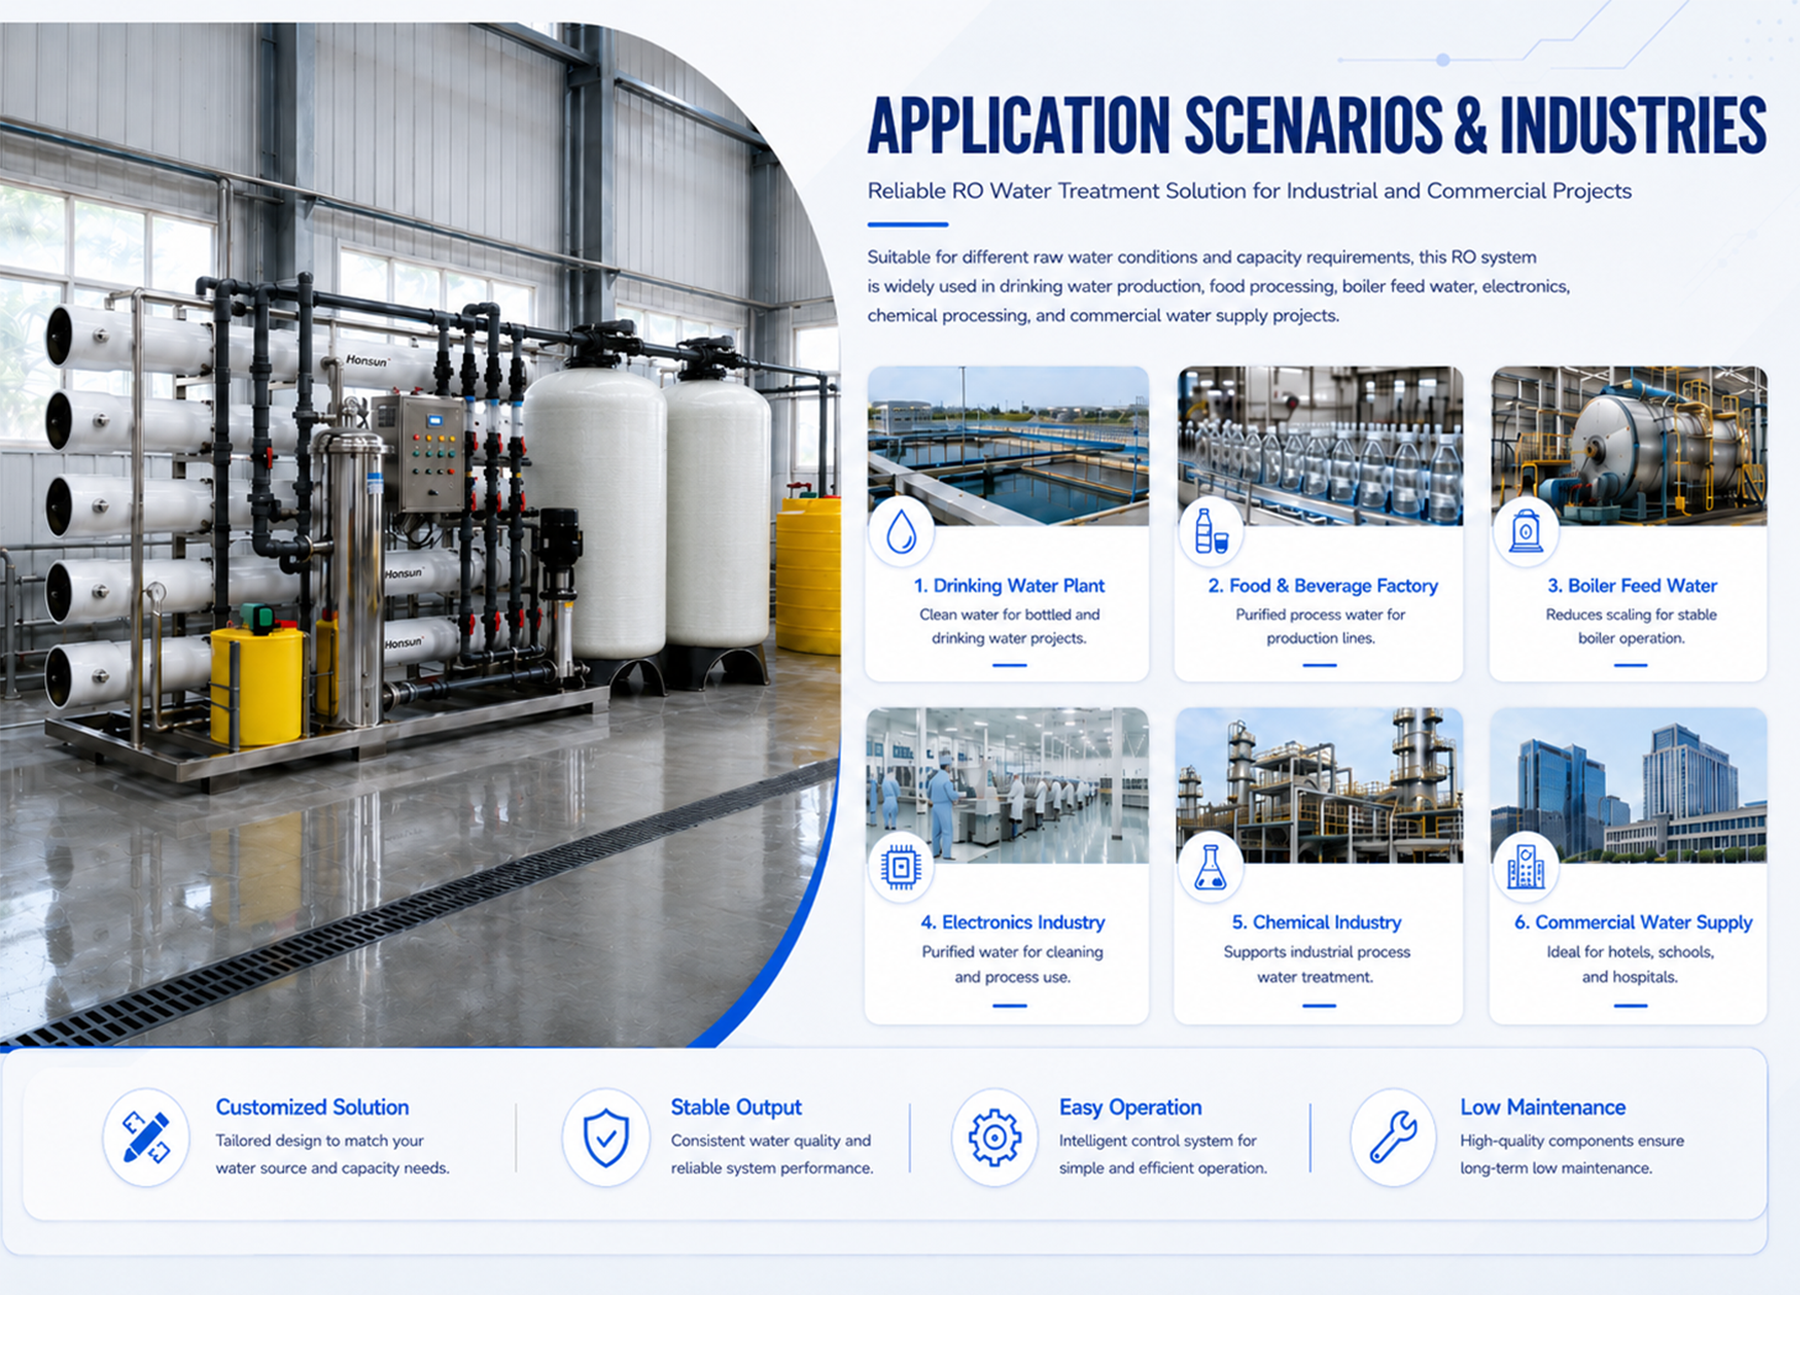
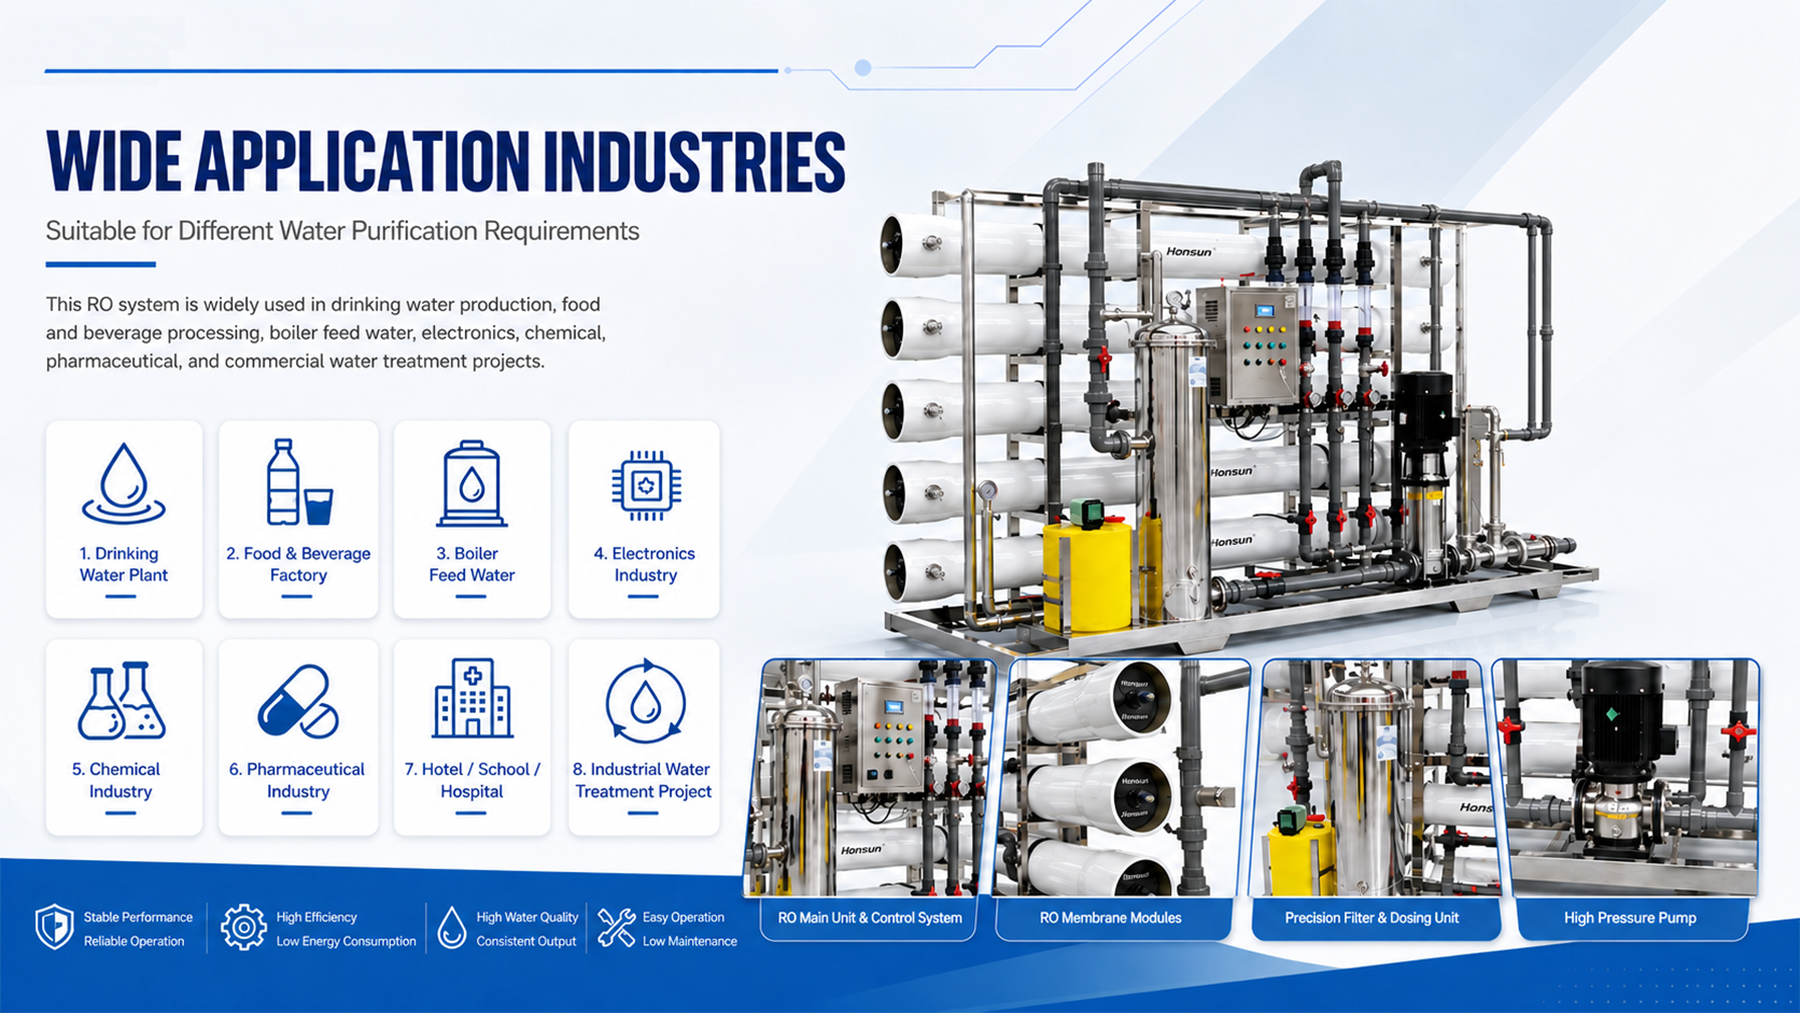
Chuangdong designs RO reverse osmosis systems specifically for the water quality requirements of the food processing industry. Our systems provide stable water quality to meet the water standards for food production.
Beverage Industry: Bottled water, fruit juice, tea drinks, carbonated beverages, beer, and craft beer. RO purified water is used for ingredient preparation and bottle and container rinsing.
Dairy Industry: Fresh milk, yogurt, milk powder, and cheese production. Applications include raw material blending, CIP (Clean-in-Place) equipment cleaning, and cooling water replenishment.
Snack Food and Condiment Industry: Sauces, soy sauce, vinegar, canned foods, preserved fruits, and baked goods. Applications include dough preparation, raw material extraction, and product formulation.
Meat and Seafood Processing: Raw material thawing and washing, marinating and brining, and hygienic cleaning of processing areas. RO water treatment helps reduce scale buildup and minimize unwanted odors.
Biotechnology and Fermentation Industry: Fermentation media preparation, extraction and purification, oral liquid production, and purified water for powdered beverage formulation.
Other Supporting Applications: RO water treatment systems can also be used for boiler feedwater pretreatment in food factories, humidification in cleanrooms, cooling water replenishment in cold storage facilities, and laboratory testing and quality control.
Conclusion
Water quality in food processing directly affects product taste, shelf life, and regulatory compliance. Whether you are building a new factory, upgrading an existing production line, or purchasing a complete water supply system, Chuangdong provides customized and reliable RO reverse osmosis systems based on your raw water quality, local regulations, and production capacity.
Fill out the form below to contact us for a customized solution, quotation, water quality assessment, and project references. We look forward to providing you with a safe and energy-efficient water treatment solution!
Frequently Asked Questions
1. What is an RO water treatment system used for in food processing?
It removes dissolved salts, heavy metals, and other impurities to provide purified water for food and beverage production.
2. Can an RO system be customized for different food factories?
Yes. We customize RO systems based on raw water quality, required water capacity, and production needs.
3. Is RO purified water suitable for beverage production?
Yes. RO water is widely used for juice blending, bottled water, tea drinks, and other beverage production processes.
4. What pretreatment is required for an industrial RO system?
Common pretreatment includes sand filtration, activated carbon filtration, and cartridge filtration. The configuration depends on the raw water quality.
5. How often should RO membranes be cleaned or replaced?
Cleaning frequency depends on water quality and operating conditions. Membrane replacement depends on performance and maintenance history.
6. Does Chuangdong provide installation and technical support?
Yes. We provide system design, equipment installation guidance, commissioning support, and technical assistance.