 EN


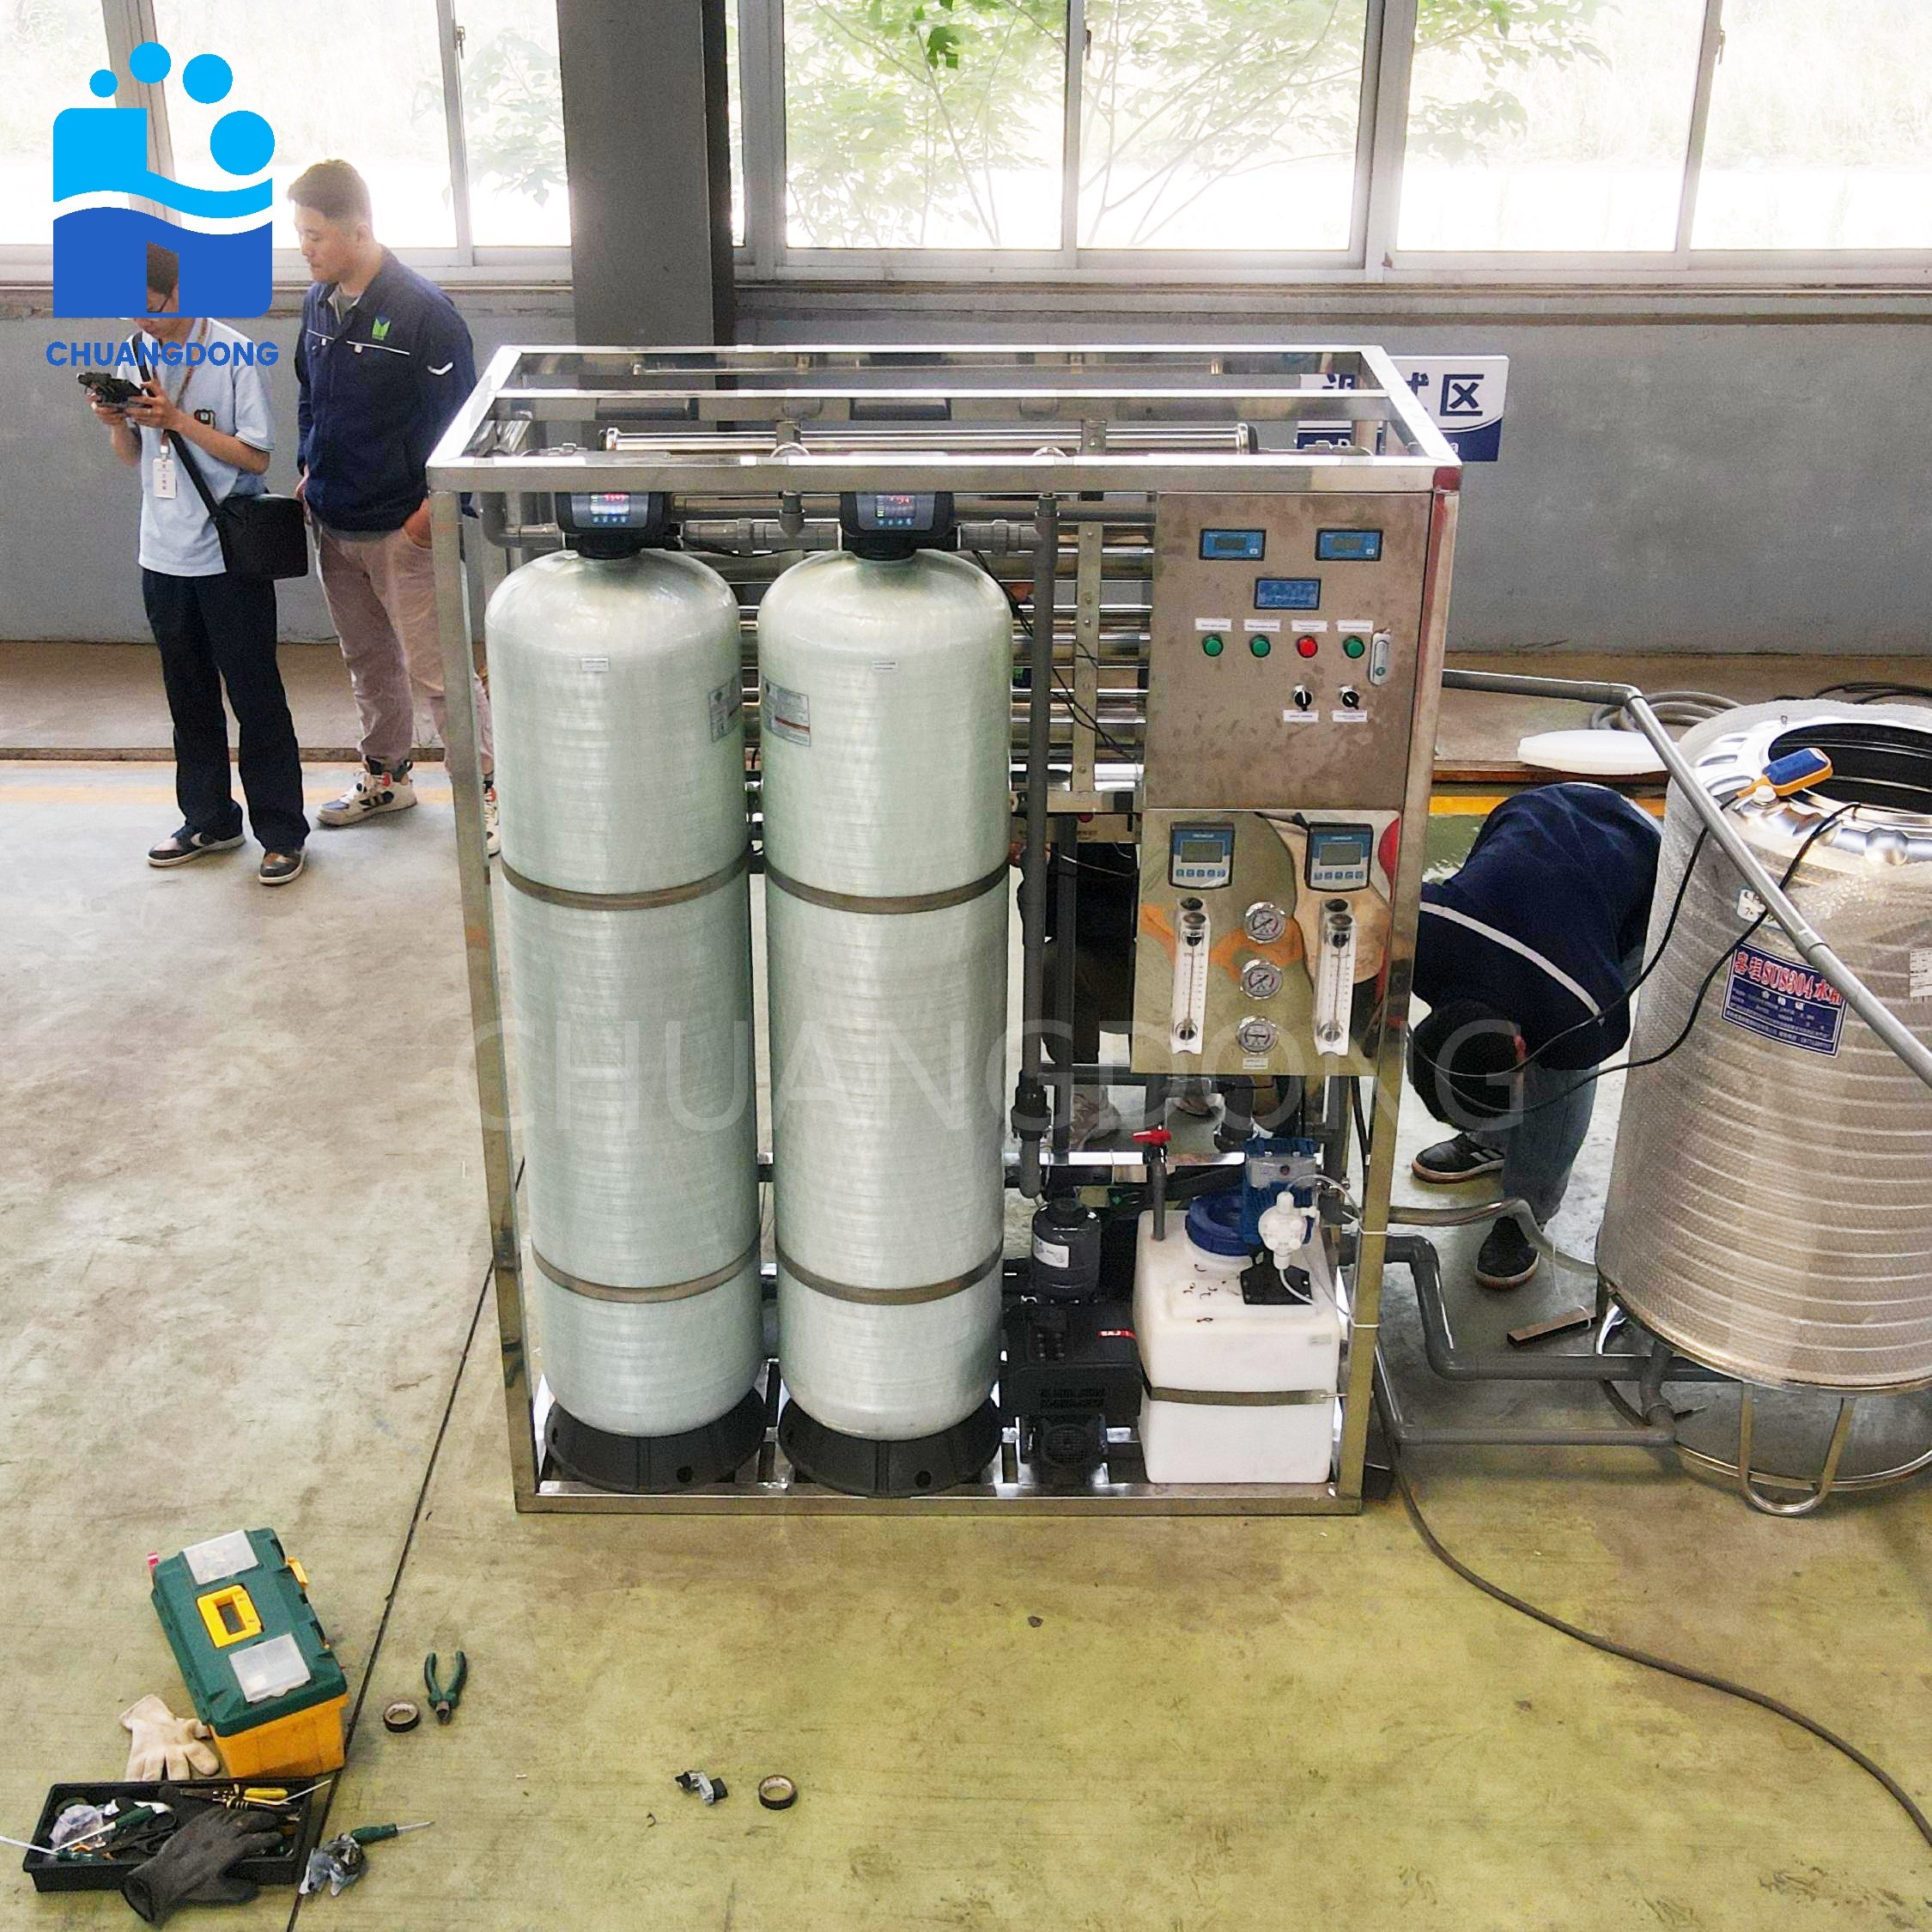
Determining the correct RO plant capacity is one of the most critical steps in designing an effective reverse osmosis water treatment system. Whether you're planning a municipal water supply, industrial process water system, or specialized purification installation, understanding how to calculate RO plant capacity ensures you invest in equipment that meets current demands while allowing for future growth. An undersized system creates bottlenecks and operational stress, while an oversized installation wastes capital and energy resources. This guide walks you through the essential calculations and considerations required to determine your optimal RO plant capacity.
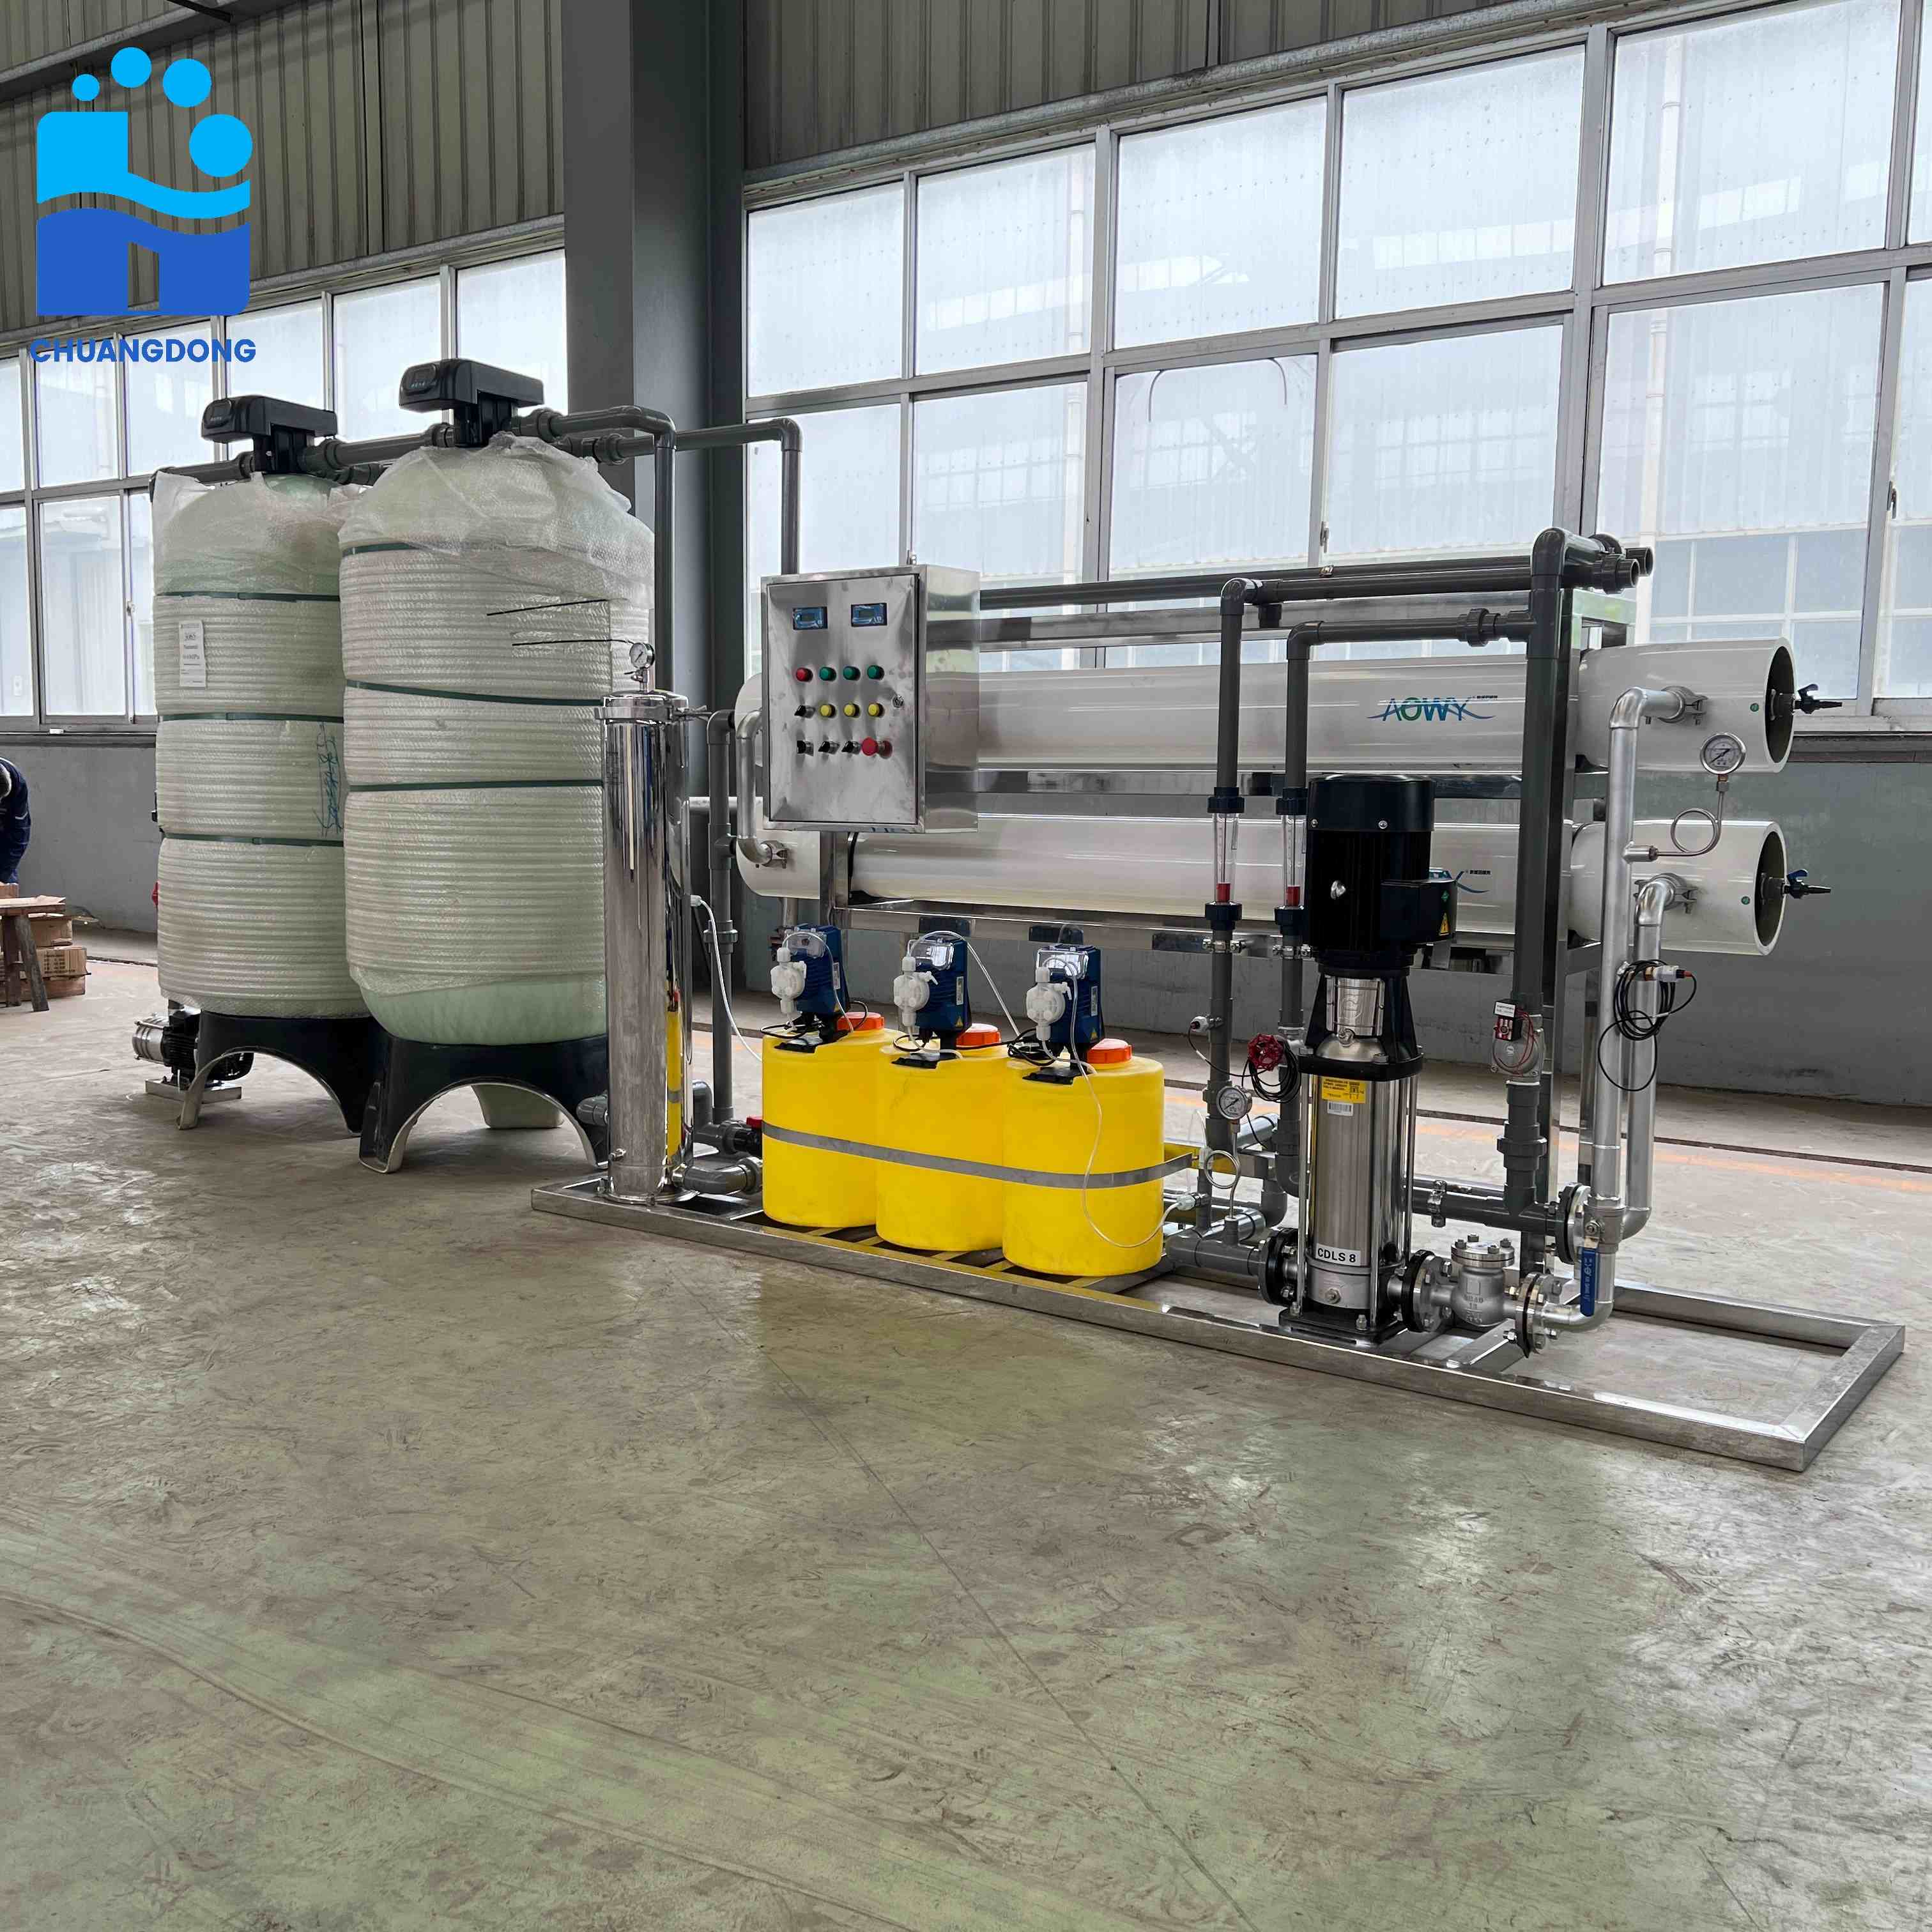
The process of calculating RO plant capacity involves multiple interconnected factors, including feed water quality, desired permeate output, recovery rates, operating pressure, and membrane specifications. The calculation isn't simply a matter of choosing a device size from a catalog. It requires careful analysis of your specific water conditions, production targets, and long-term operational strategy. By mastering the fundamentals of RO plant capacity determination, you position your facility for reliable, cost-effective water treatment performance.
Understanding Feed Water Characteristics and Quality Parameters
Role of Total Dissolved Solids (TDS) in RO plant capacity Calculations
The composition of your feed water directly influences how much RO plant capacity you'll need and what design modifications may be required. Total Dissolved Solids (TDS) represents all inorganic salts, minerals, and dissolved substances in water. High-TDS feed water creates greater osmotic pressure resistance, which affects the power requirements and effective throughput of your RO plant capacity system. If your feed water contains 2,000 mg/L TDS, the system requires significantly more pressure and energy than feed with 500 mg/L TDS to achieve the same RO plant capacity output. Pre-filtration, cartridge filters, and media filters help reduce suspended solids that could damage membranes and reduce effective RO plant capacity performance.
Scaling Potential and Fouling Concerns Affecting System Output
Beyond TDS levels, specific ions like calcium, magnesium, silica, and barium can form scale deposits on membrane surfaces, reducing functional RO plant capacity over time. When planning your RO plant capacity, you must account for fouling frequency, which may require either higher system sizing to compensate for gradual capacity loss between cleanings, or more frequent maintenance cycles. Water softening pre-treatment can extend the operating efficiency of your RO plant capacity installation. Understanding your water's Saturation Index (SI) and Langelier Index (LI) helps predict scaling likelihood and adjust your target RO plant capacity accordingly.
Core Calculation Methods for Determining RO plant capacity
The Recovery Rate Formula and Its Impact on RO plant capacity
Recovery rate is the percentage of feed water converted into usable permeate. The fundamental formula for calculating RO plant capacity involves three variables: Feed Flow Rate (F), Recovery Rate (R), and Permeate Flow Rate (P). The relationship is expressed as P = F × R. If you need 100 gallons per minute (GPM) of permeate water and your system operates at a 75% recovery rate, your feed water supply must deliver approximately 133 GPM. This inverse relationship between recovery rate and feed requirement directly determines the actual RO plant capacity you must purchase. Higher recovery rates reduce feed water demand but increase concentrate disposal challenges. Most industrial RO plant capacity installations operate between 50% and 85% recovery, depending on feed water quality and end-use requirements.
Determining Concentrate Flow and Multi-Pass System Design
The concentrate or reject stream from your RO plant capacity system flows away at a rate calculated as C = F - P. If feed is 133 GPM and permeate is 100 GPM, concentrate equals 33 GPM. Managing this concentrate stream affects your actual usable RO plant capacity because disposal costs and environmental regulations may require you to recirculate or treat it further. Two-pass RO systems treat first-pass permeate through a second set of membranes, effectively increasing overall RO plant capacity purity but at the expense of additional equipment cost and energy consumption. When calculating total system RO plant capacity, account for whether your process requires single-pass or multi-pass treatment architecture.
Operational Factors and Real-World Performance Considerations
Accounting for Temperature, Pressure, and Membrane Age Effects on RO plant capacity
Temperature significantly influences membrane permeability and osmotic pressure dynamics. For every 1°C increase above reference temperature, RO membrane productivity typically increases by 2% to 3%. This means your calculated RO plant capacity rating assumes operation at a specific reference temperature, often 25°C. In cold climates or seasonal variations, your actual RO plant capacity output may fall 15% to 20% below nominal ratings. Operating pressure, measured in pounds per square inch (PSI), must exceed the feed water's natural osmotic pressure to force water molecules across the membrane. Typical RO plant capacity systems operate between 150 and 300 PSI depending on feed water salinity and desired recovery. As membranes age and accumulate minor fouling, operating pressure must increase to maintain the same RO plant capacity output, reducing overall system efficiency until cleaning or replacement becomes necessary.
Capacity Derating and Safety Margins in RO plant capacity Sizing
Manufacturers typically rate RO plant capacity under ideal laboratory conditions using clean water at standardized temperature and pressure. Real-world applications require a derating factor, usually between 0.8 and 0.95, applied to nameplate capacity. This accounts for temperature variations, minor membrane fouling, pressure drop through pipes and fittings, and normal operational inconsistencies. A system rated at 1,000 GPD RO plant capacity might realistically deliver 800 to 950 GPD under typical field conditions. Wise facility managers calculate required RO plant capacity by applying a 1.2 to 1.3 safety factor to their minimum daily demand, ensuring the system can handle peak loads and accommodate future growth without operating at maximum capability continuously. This approach extends membrane life and maintains operational reliability as your RO plant capacity gradually declines over its service life.
Practical Design Example and Implementation Strategy
Step-by-Step RO plant capacity Calculation for an Industrial Facility
Consider a manufacturing facility requiring 500 gallons per day (GPD) of purified water for process cooling and equipment washing. The facility's feed water tests at 1,200 mg/L TDS and operates at ambient temperature varying between 10°C and 30°C. Using a conservative 75% recovery rate and applying a 1.25 safety factor to account for seasonal temperature swings, the required RO plant capacity is calculated as follows: Base demand of 500 GPD multiplied by 1.25 safety factor equals 625 GPD required permeate. Dividing 625 GPD by 75% recovery rate yields 833 GPD feed water requirement. At 10°C operation, accounting for 15% capacity loss due to temperature effect, the facility should specify a RO plant capacity system rated at approximately 975 GPD under standard conditions. This ensures adequate output during cold months while allowing headroom for membrane aging and future production increases.
Selecting Membrane Configuration to Optimize Effective RO plant capacity
Once you've calculated required RO plant capacity, you must select the right membrane element size and quantity. Common RO membranes are available in 2.5-inch and 4-inch diameters, with different area ratings from 150 to 400 square feet per element. Larger diameter membranes offer higher RO plant capacity per element but require proportionally larger pressure vessels and higher capital investment. Membrane quantity and arrangement in series or parallel affects both RO plant capacity and concentrate management. A single-pass 4-inch membrane configuration might deliver your required RO plant capacity efficiently for municipal supply applications. However, ultra-high-purity applications like semiconductor manufacturing or pharmaceutical production may require two or three stages of RO, with each stage's RO plant capacity carefully calculated to balance overall system efficiency, water recovery, and final product quality specifications.
FAQ
What is the most important factor when calculating RO plant capacity?
The recovery rate is arguably the most critical factor because it directly determines how much feed water your facility must supply to achieve desired permeate output. The recovery rate depends on your feed water quality, desired water purity, and concentrate disposal constraints. A small error in selecting recovery rate cascades through all downstream calculations of RO plant capacity, affecting equipment size, capital cost, and operational expenses significantly.
How does temperature affect my system's RO plant capacity performance?
Temperature variations can change actual RO plant capacity output by 2% to 3% per degree Celsius from the reference temperature. Cold feed water reduces membrane productivity and effective RO plant capacity, while warm water increases it. When calculating RO plant capacity for facilities with seasonal water temperature fluctuations, apply appropriate safety factors or consider heated or cooled feed pre-treatment to maintain consistent system performance year-round.
Should I size my RO plant capacity based on average demand or peak demand?
Always base RO plant capacity sizing on peak demand plus a safety margin, typically 1.2 to 1.3 times the maximum hourly requirement. Sizing only to average demand creates bottlenecks during peak usage periods and forces the system to operate at maximum pressure continuously, accelerating membrane fouling and reducing service life. The additional capital investment in oversizing for peaks is far less expensive than operational inefficiency, product quality issues, or premature membrane replacement due to sustained stress operation.